Sintered Bushing & Bearing | Oil-Impregnated Bronze & Iron
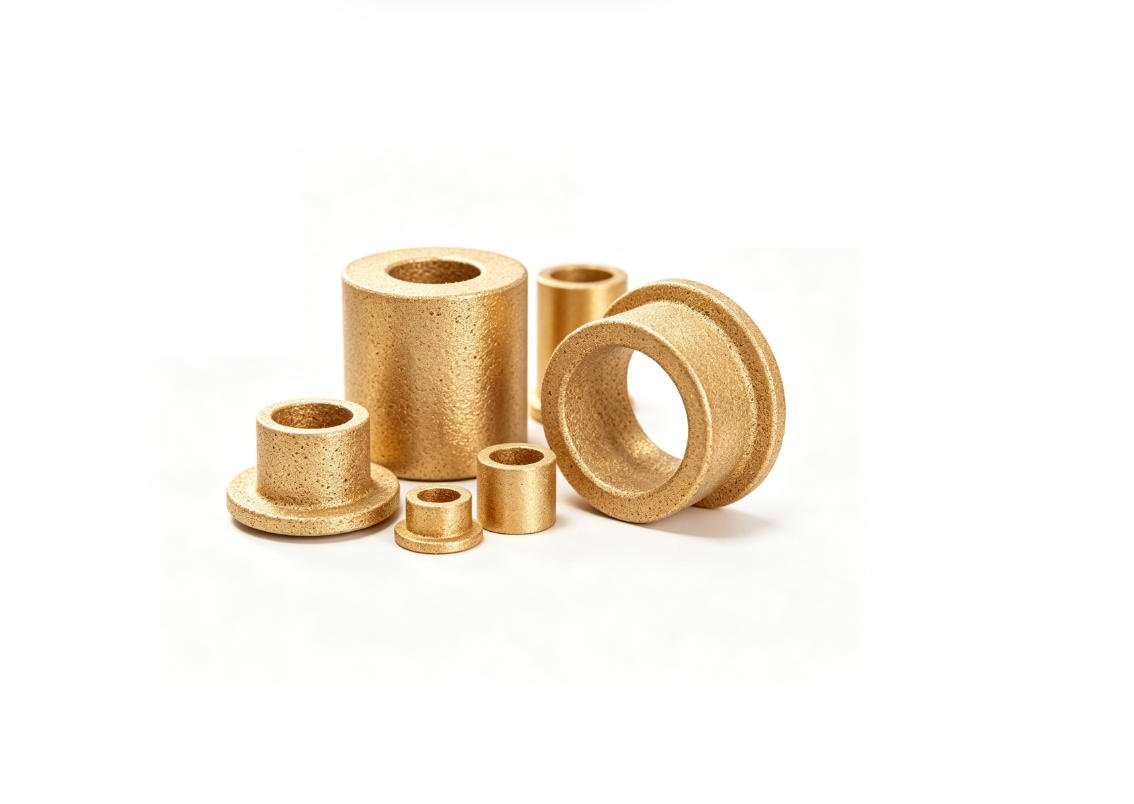
A sintered bushing is a porous metal sleeve made by pressing metal powder in a die and sintering it in a furnace, then vacuum-filled with 10-20% oil by volume. The oil sweats out as the bushing heats during operation and reabsorbs when it cools. We make tin-bronze (Cu-Sn 90/10), iron-copper and stainless (316L, 17-4 PH) versions in cylindrical, flanged, thrust and spherical shapes, in 5.6-6.8 g/cm³ density. The bushing runs 3,000-5,000 hours without external lubrication, and is the most common PM bearing for power tools, home appliances, textile machines, automotive gearboxes and industrial equipment.
In-house PM line at our IATF 16949 factory in Ningbo: 16 compaction presses, 10 sintering furnaces, 3 Zeiss CMMs. Cylindrical, flange, thrust, spherical and specialty variants – drop-in replacement for machined bronze at lower cost. Tooling in about 20 days, first-article samples in 25, DFM review within 48 hours.
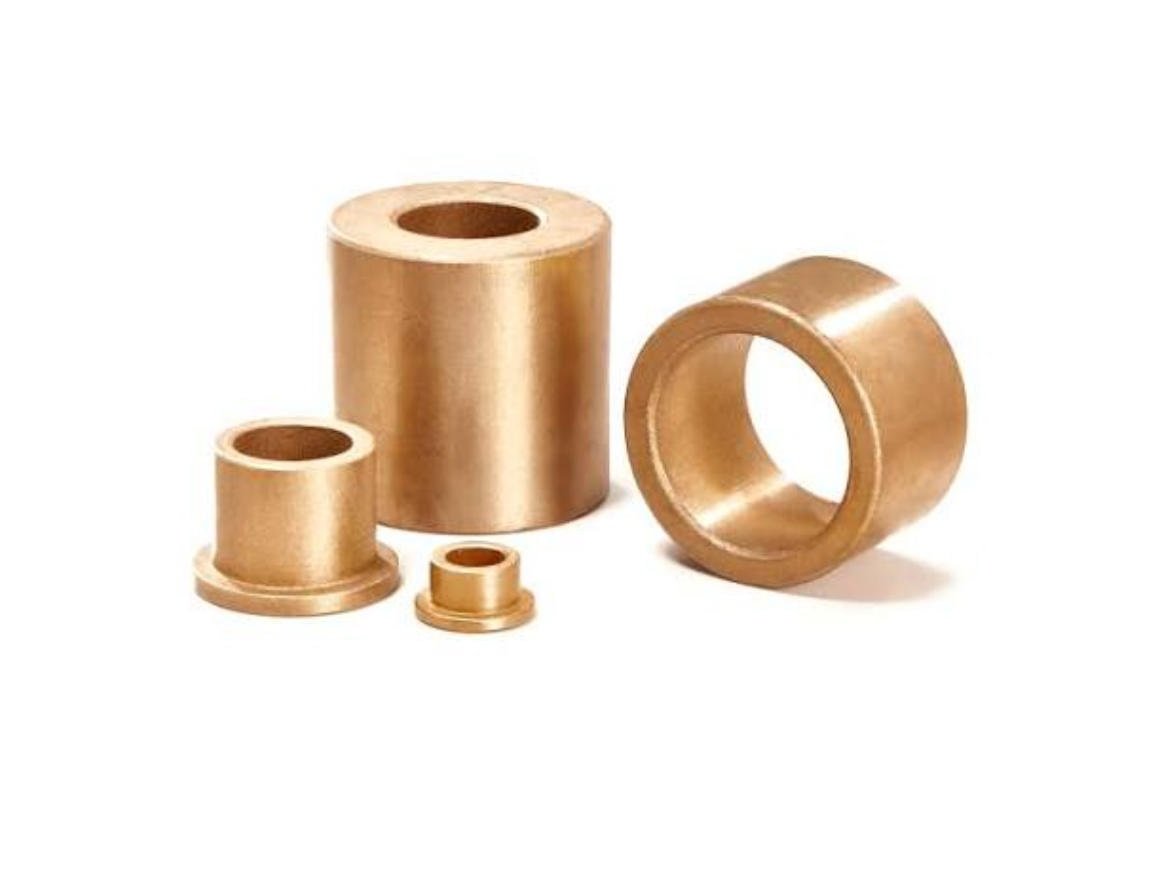
We make – PM is well-suited here
- Oil-impregnated cylindrical sintered bushings in bronze, iron, steel
- Sintered flange bushings and thrust washers
- Spherical and self-aligning sintered bushings
- PTFE- or graphite-impregnated variants for long-life / low-friction duty
- Custom bore / OD / length against your housing drawing or sample
- Stainless 316L / 17-4PH for food-grade, marine or corrosive service
We don’t make – ask a partner shop
- Rolling-element ball / roller bearings (not a PM part – use NSK / SKF / FAG)
- Solid (non-porous) bronze or brass bushings (use machined bar stock)
- Ceramic bearings (Si3N4, ZrO2 – use a ceramic bearing maker)
- Rubber-lined water-lubricated bearings (use a marine bearing maker)
Need a rolling-element bearing or ceramic race? Ask us anyway – we partner with bearing distributors in Ningbo and can quote the full kit under one PO. Tell us what you need.
Sintered bushing vs machined bronze vs rolling bearing
The three most common bearing choices for the same shaft. Pick by load, speed and how often you want to re-grease.
| Parameter | Sintered bushing (PM) | Machined bronze bushing | Rolling-element bearing |
|---|---|---|---|
| Typical service life | 3,000-5,000 hours, no relubrication | 5,000-10,000 hours, requires re-greasing | 10,000-50,000 hours, sealed or regrease |
| Maximum running speed | ~3,500 rpm (bronze), ~5,000 rpm (iron) | ~5,000 rpm with full film lubrication | 10,000+ rpm depending on series |
| Load capacity (radial) | Medium – 20-80 MPa | Medium – 30-100 MPa | High – 100-500+ MPa |
| Maintenance | None (oil-impregnated) | Re-grease every 500-1,000 hours | Re-grease every 2,000-5,000 hours or sealed-for-life |
| Cost per piece (relative) | Low – typical for PM volume | Medium – high machining time | High – precision-ground races |
| MOQ for custom sizes | 2,000 pcs at JH PM | 500-1,000 pcs | 1-100 pcs (catalogue sizes) |
| Tooling lead time (custom) | ~20 days | ~15-25 days | Not applicable – catalogue only |
| Best for | Sealed housings, slow / medium speed, low maintenance | Open gearboxes, oil-bath lubrication | High speed, high precision, long life |
| Our recommendation | Default for power tools, appliances, textile looms, low-cost gearboxes | Use only when oil bath is available | Use when speed or precision dominates cost |
Four sintered bushing and bearing families we make
Each cluster below groups the part geometries we run most often. Click through to the part card for typical dimensions, materials and tolerances.
Cylindrical Sintered Bushings
Cylindrical sleeve bushings – the workhorse of self-lubricating PM bearings. Tin-bronze, iron-copper and stainless. OD 10-120 mm, length 5-80 mm.
Flange Bushings & Thrust Washers
Flanged bushings hold axial position in the housing; thrust washers support axial load on a shaft shoulder. Bronze, iron, stainless.
Spherical & Self-Aligning Bushings
Spherical sintered bushings – the inside diameter is ground spherical to compensate for shaft misalignment. Used in suspension, take-up rolls and rocker arms.
Specialty Bearings & Pre-Matched Kits
Stainless variants for food / marine, PTFE-impregnated for low-friction long-life, graphite-impregnated for high-temperature. Also bearing kits (bushing + matched thrust washer) under one P/N.
Cylindrical Sintered Bushings – Range & Materials
Cylindrical sleeve bushings are the default PM bearing shape. They drop into a housing bore and run on a shaft, releasing stored oil as they heat up. We size them to your drawing or sample, with three standard material families covering most industrial duty.
From our quoting desk: roughly 1 in 5 RFQs we see is for an iron-copper bushing running above 5,000 rpm. They fail early in that range. Above 5,000 rpm we push customers to tin-bronze or to a rolling bearing – whichever fits the cost target.
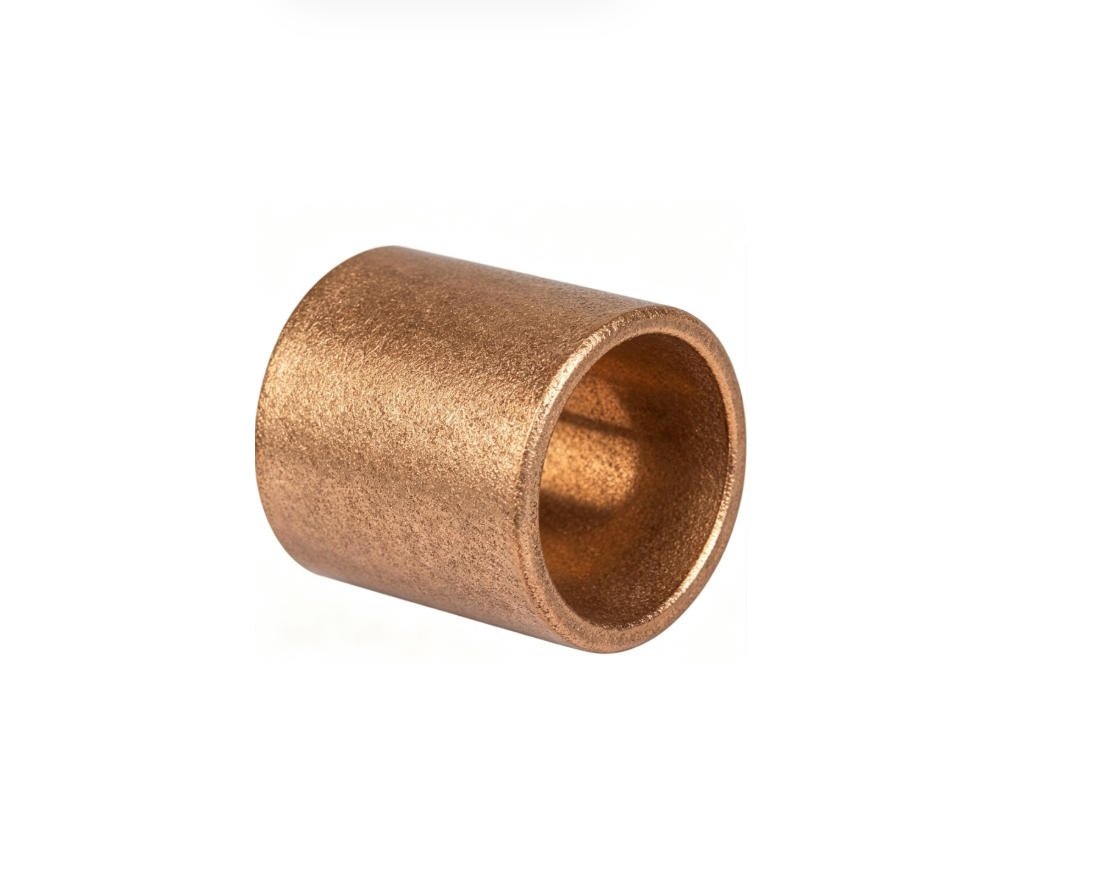 Oil-impregnated sintered bronze bushing
Cu-Sn 90/10, density 6.0-6.8 g/cm³, oil 12-18% vol. OD 10-80 mm, length 5-60 mm. Up to ~3,500 rpm.
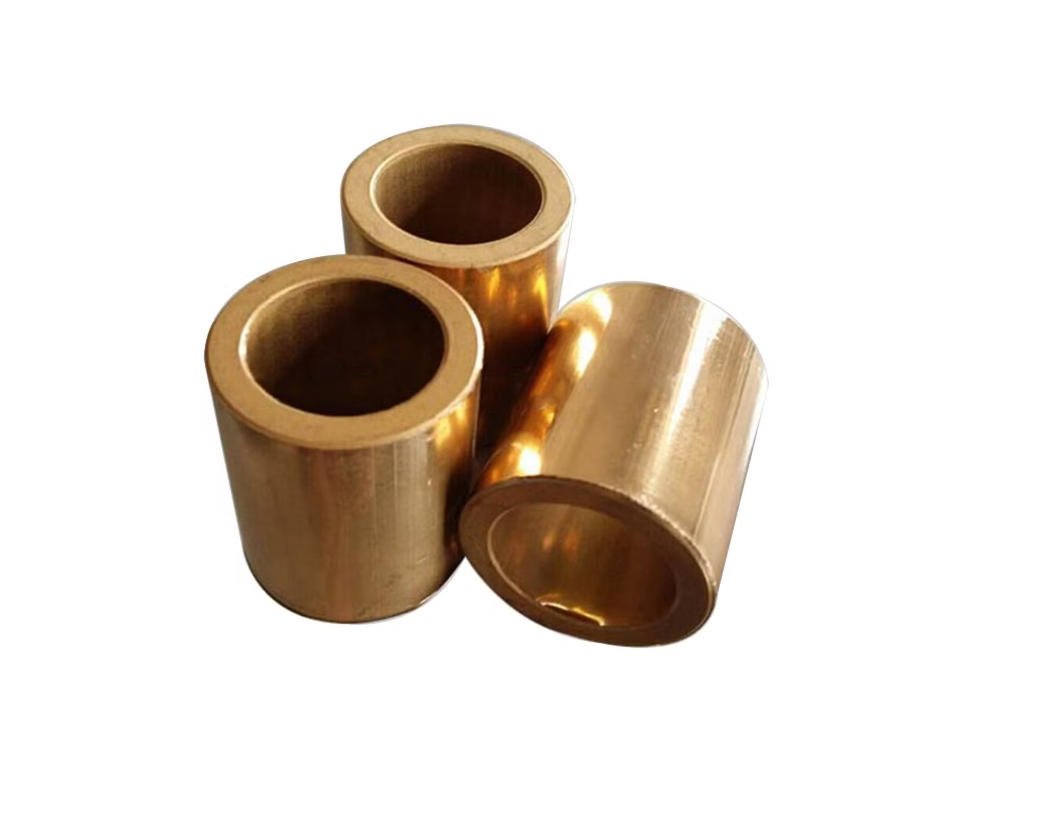 Sintered iron bushing (Fe-Cu)
Fe-Cu, density 5.8-6.5 g/cm³, oil 10-15% vol. OD 12-100 mm, length 6-70 mm. Higher load, lower cost than bronze.
Flange Bushings & Thrust Washers – Where Axial Load Matters
Flanged bushings locate the bearing axially in the housing without a separate retainer; thrust washers support axial load on a shaft shoulder. Both come in bronze, iron-copper and stainless and are oil-impregnated the same way as cylindrical bushings.
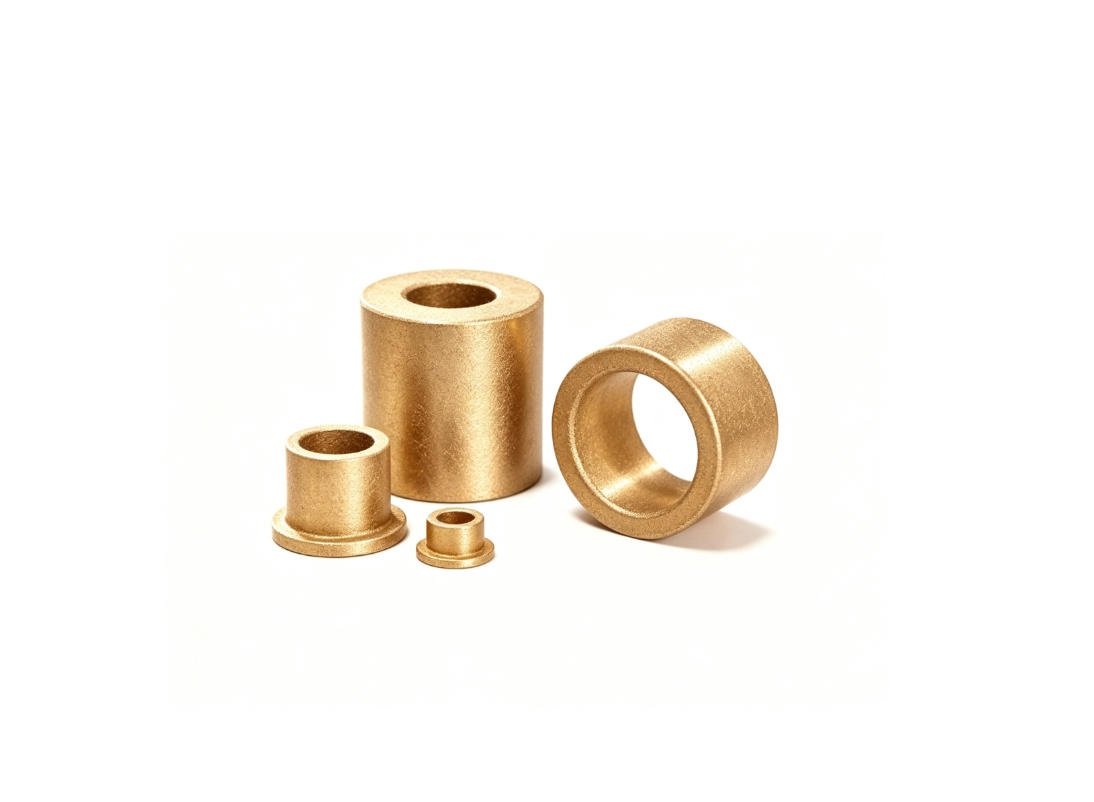 Sintered bronze flange bushing
Cu-Sn bronze, flange OD 18-120 mm. Common in washing-machine motor, fan motor, hand-tool gearbox.
 Sintered iron thrust washer
Fe-Cu iron thrust washer, OD 20-100 mm, thickness 2-8 mm. Supports axial load in gearboxes and pump housings.
Spherical & Self-Aligning Sintered Bushings
Spherical sintered bushings have a spherical inner bore, so the bearing self-aligns with the shaft and compensates for misalignment up to about 5°. Common in suspension pivots, rocker arms, hydraulic cylinder rod ends and take-up rolls.
Real failure mode we see: spherical bushings fail when the misalignment is sustained, not when it is brief. A suspension pivot on a slow-moving arm is fine. A high-cycle hydraulic rod end at 60 cycles / minute wears the bronze race in 1,500-2,000 hours. For that duty, switch to PTFE-impregnated.
Specialty Bearings & Pre-Matched Kits
Material variants and assembled kits for conditions outside the standard oil-impregnated envelope: stainless for corrosion, PTFE for low friction, graphite for high temperature. Also pre-matched bushing + thrust washer kits under one P/N.
Capabilities for sintered bushings and bearings
What you can ask for in your RFQ. All numbers are in-house, not subcontracted.
What we see in real RFQs: wall thickness below 1.2 mm is the single most common reason we reject a drawing. The bushing cracks during ejection. Warm pressing solves it but doubles the tooling cost. If wall thickness is tight, flag it on the drawing before we start.
| Parameter | Standard range | Notes |
|---|---|---|
| Materials | Cu-Sn 90/10, Fe-Cu, Fe-Cu-Ni-Mo, 316L stainless, 17-4 PH stainless | Material certificate per lot |
| Density (Cu-Sn) | 6.0 – 6.8 g/cm³ | Higher density = higher load capacity |
| Density (Fe-Cu) | 5.8 – 6.5 g/cm³ | Iron-copper grade, lower cost |
| Density (stainless) | 5.6 – 6.4 g/cm³ | 316L / 17-4 PH, food-grade / marine |
| Oil content | 10 – 20% vol. (ISO VG 32 / 46 / 68 standard) | Customer-specified oil on request |
| OD range | approx. 10 – 120 mm | 500 t PM press envelope |
| Length range | approx. 5 – 80 mm | Long parts: split-press multi-level |
| Bore tolerance | ISO JS7 standard; ISO JS6 on sized bushings | Ground bore on request |
| Wall thickness | min 1.5 mm; typical 2-6 mm | Thin wall below 1.5 mm needs warm pressing |
| Specialty impregnation | PTFE, graphite, food-grade oil, high-temp oil | Selected per your duty |
| MOQ | 2,000 pcs | Lower for sampling / replacement lots on request |
| Tooling lead time | approx. 20 days | In-house die + mandrel + EDM |
| Sample lead time | approx. 25 days after tooling approval | FAI report included |
| DFM review | 48 hours | Written DFM note against your drawing |
| QC | 3 Zeiss CMMs, density meter, oil-content test, bore gauge | Lot-level MES traceability |
| Certifications | IATF 16949:2016, ISO 9001:2015 | Audited annually by SGS |
| Common HS code | 7326 (other articles of iron/steel) / 7415 (copper articles) / 8483 (transmission parts) – confirm with your broker for the specific line on your commercial invoice | For customs declaration |
How a sintered bushing is made at JH PM
Six steps from your drawing to an oil-impregnated lot. Same process we use for our automotive and power-tool bearings – just a different press cycle and a different oil.
On oil choice: we default to ISO VG 46 mineral oil for general-purpose bushings, VG 32 for low-temperature or high-rpm duty, VG 68 for slow-speed high-load housings. If your application is food-grade, food-grade white oil is available. If you have a specific oil specified by your design, send the data sheet with the drawing.
FAQ – Sintered bushings and bearings
What is a sintered bushing?
A sintered bushing – also called a sintered bearing, oil-impregnated bushing or self-lubricating bushing – is a porous metal sleeve made by compacting metal powder in a die and sintering it in a furnace. The connected porosity is then vacuum-impregnated with 10-20% lubricating oil by volume. The bushing releases oil as it heats during operation and reabsorbs it when it cools, giving 3,000-5,000 running hours of maintenance-free service without external lubrication.
What materials are used for sintered bushings and bearings?
Three material families cover most industrial sintered bushing and bearing applications: tin-bronze (Cu-Sn, the most common, used for general-purpose self-lubricating bearings up to about 3,500 rpm), iron-copper (Fe-Cu, higher load capacity and lower cost, used in automotive gearboxes and power tools), and stainless (316L for food-grade and marine, 17-4PH for high-temperature or corrosive duty). We hold 5.6-6.8 g/cm³ density across the three families depending on the material and the load class. Sintered bronze bearing variants typically use the tin-bronze 90/10 alloy as the base composition.
What density and oil content do you hold on a sintered bushing?
On tin-bronze sintered bushings we hold 6.0-6.8 g/cm³ density with 12-18% oil content by volume. On iron-copper sintered bushings we hold 5.8-6.5 g/cm³ density with 10-15% oil content. The exact target depends on the load class and the running speed; our DFM review includes a density / oil content recommendation against your housing and shaft dimensions.
Can a sintered bronze bushing run dry, without external oil?
Yes – that is the main reason customers specify sintered bronze bushings instead of machined bronze. The oil stored inside the porous structure continuously feeds the shaft-bore interface, so the bushing runs maintenance-free for 3,000-5,000 hours. For applications above about 5,000 hours, or where a low-viscosity oil film is critical, we recommend PTFE-impregnated or graphite-impregnated variants – send a drawing for a tailored recommendation.
What is the difference between a sintered bushing and a sintered bearing?
In B2B usage the two terms overlap: a bushing is a cylindrical plain bearing (sleeve) used in a housing to support a shaft, and a bearing is the broader category that includes bushings plus flange bushings, thrust washers, spherical bushings and ball-bearing races. A ‘sintered bearing’ is almost always a sintered plain bearing – i.e. a bushing – because rolling-element bearings are not made by PM pressing. We make all the common sintered bearing geometries: cylindrical, flanged, thrust washer, spherical.
What is the typical MOQ and lead time for a custom sintered bushing?
MOQ starts at 2,000 pieces for custom dimensions. Tooling is around 20 days, first-article samples in about 25 days after tooling approval. For breakdown spares or sampling against an existing part, we keep a buffer of common bushing geometries – send your drawing or a sample and we will quote a 5- to 10-day expedite on what we can match.
What oil viscosity options are available for oil-impregnated sintered bushings?
We default to ISO VG 46 mineral oil for general-purpose bushing duty, VG 32 for low-temperature or higher-speed housings, and VG 68 for slow-speed high-load housings. We can also impregnate with food-grade white oil, synthetic PAO or customer-specified oil against a data sheet. Oil content is set at 12-18% by volume for tin-bronze and 10-15% for iron-copper. Saturated weight and oil grade are recorded on every MTC.
Do you provide PPAP, IMDS and RoHS documentation with sintered bushing shipments?
Yes. For automotive programs we supply a full PPAP package: design records, material certificates, dimensional FAI, Cpk data on critical features, and process flow diagrams. We submit IMDS entries for all iron-copper and steel grades. RoHS and REACH compliance statements are issued on request, with test reports from SGS where the customer requires third-party verification. For non-automotive customers we still issue an MTC with density, oil content and dimensional data on every lot.
Have a sintered bushing or bearing in mind?
Send a drawing, a sample or your housing / shaft dimensions and get a DFM review within 48 hours. We make oil-impregnated bronze, iron and stainless bushings, flange bushings, thrust washers, spherical bushings and PTFE / graphite-impregnated variants. For rolling-element bearings, ask us anyway – we partner with bearing distributors in Ningbo.
Request a Quote