Sintered power tool parts built for gearboxes that never stop.
JH PM is a powder-metal factory in Ningbo, China. We press, sinter, and finish-machine gears, pinions, planetary sets, and clutch components for cordless drills, impact drivers, angle grinders, hammer drills, and rotary hammers. IATF 16949 since 2018, 19 PM presses (60–800 t), 10 sintering furnaces, and a closed-loop material-traceability system.
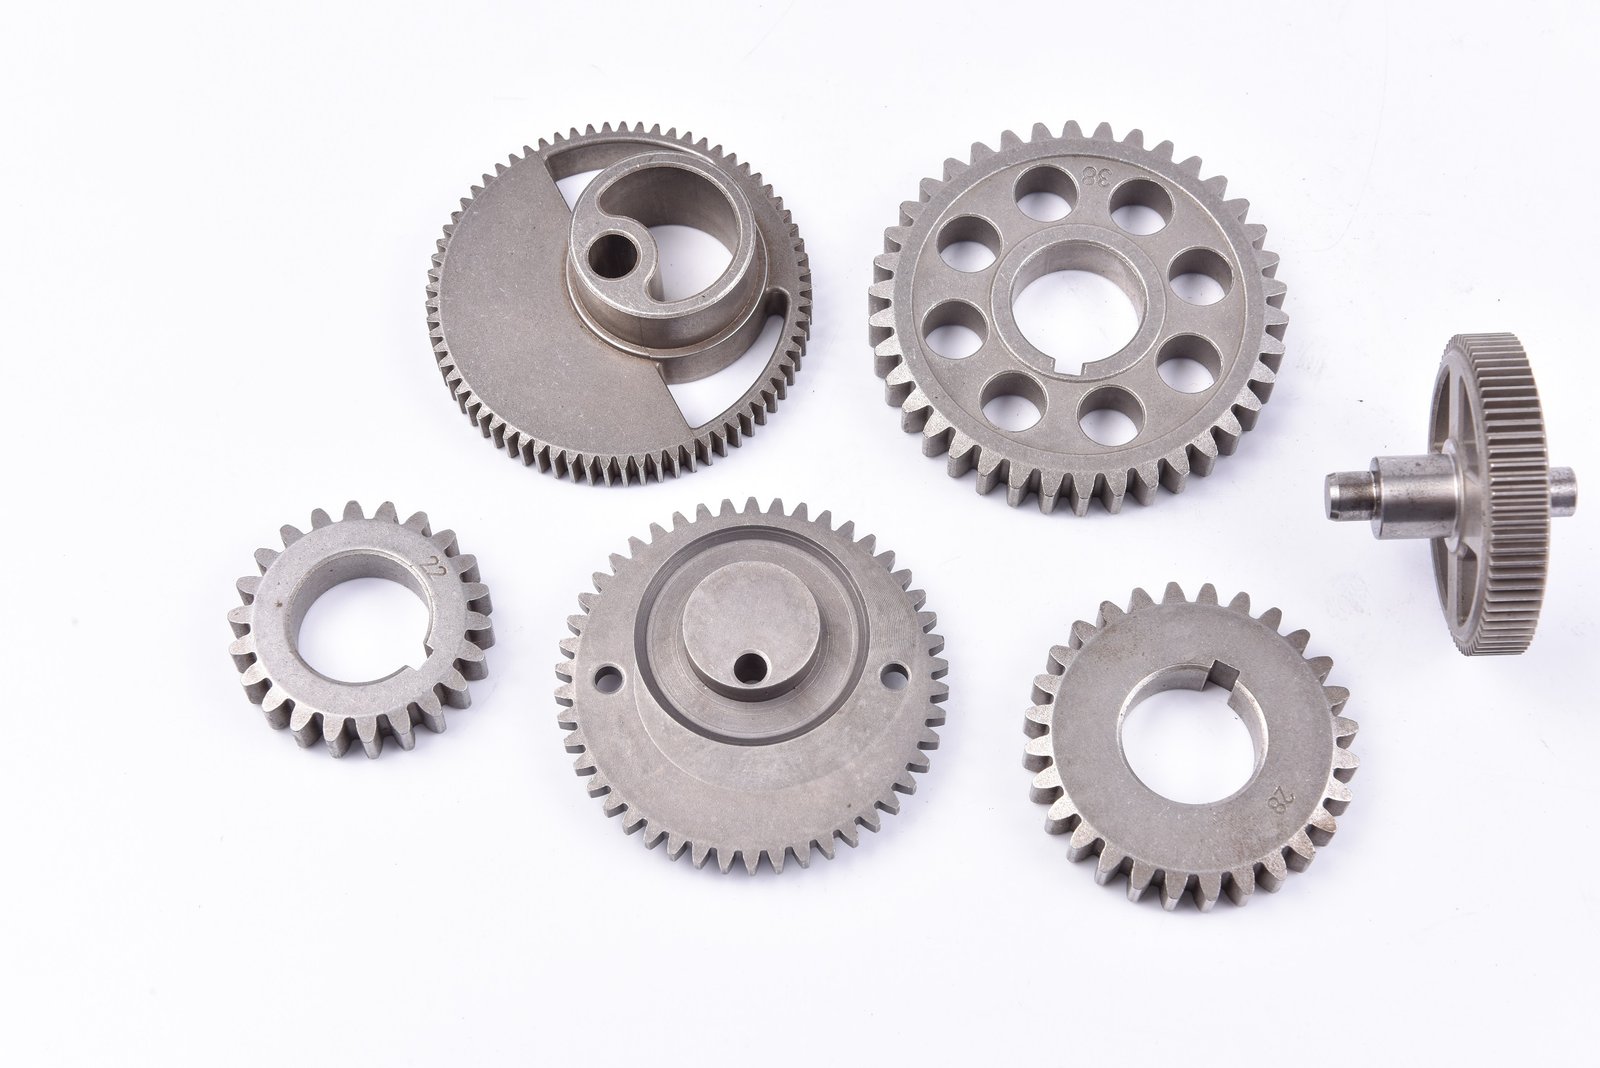
Four part families covering the most common power-tool gear trains.
Each family is built on a different press-and-sinter flow, so the density, hardness, and post-machining window are tuned to the part’s load case. We don’t sell catalog gears; we engineer the powder blend, compaction curve, and finish-machining plan around your drawing.
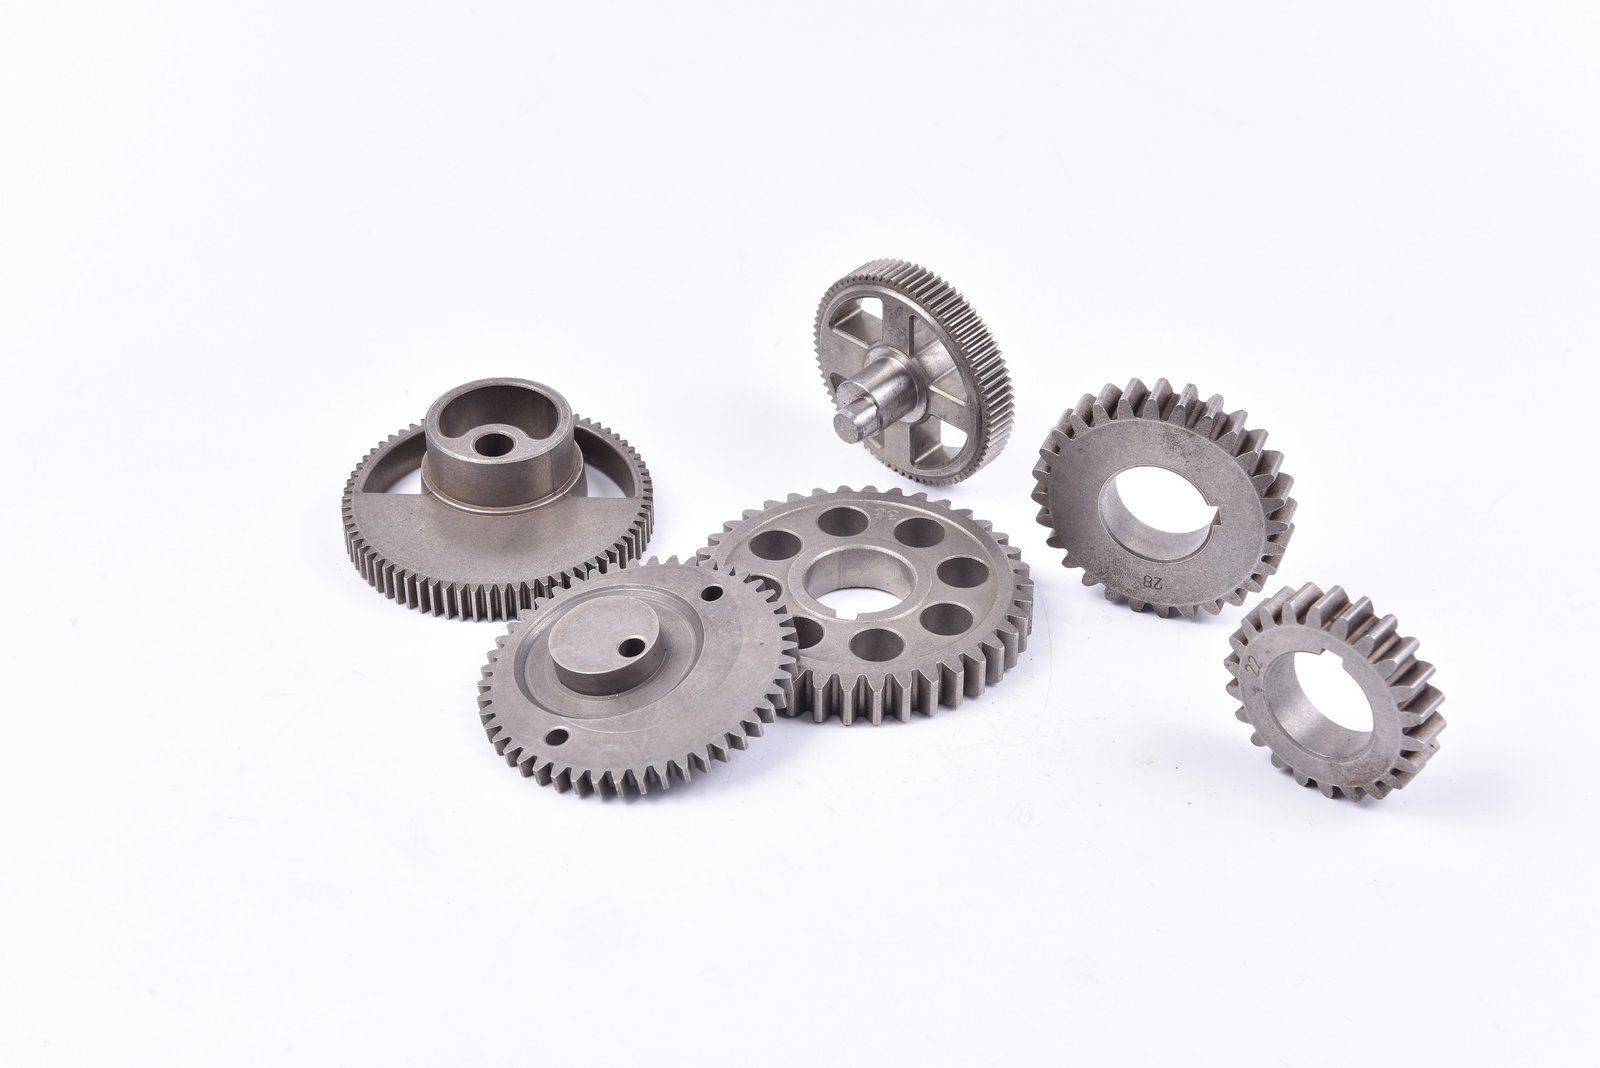
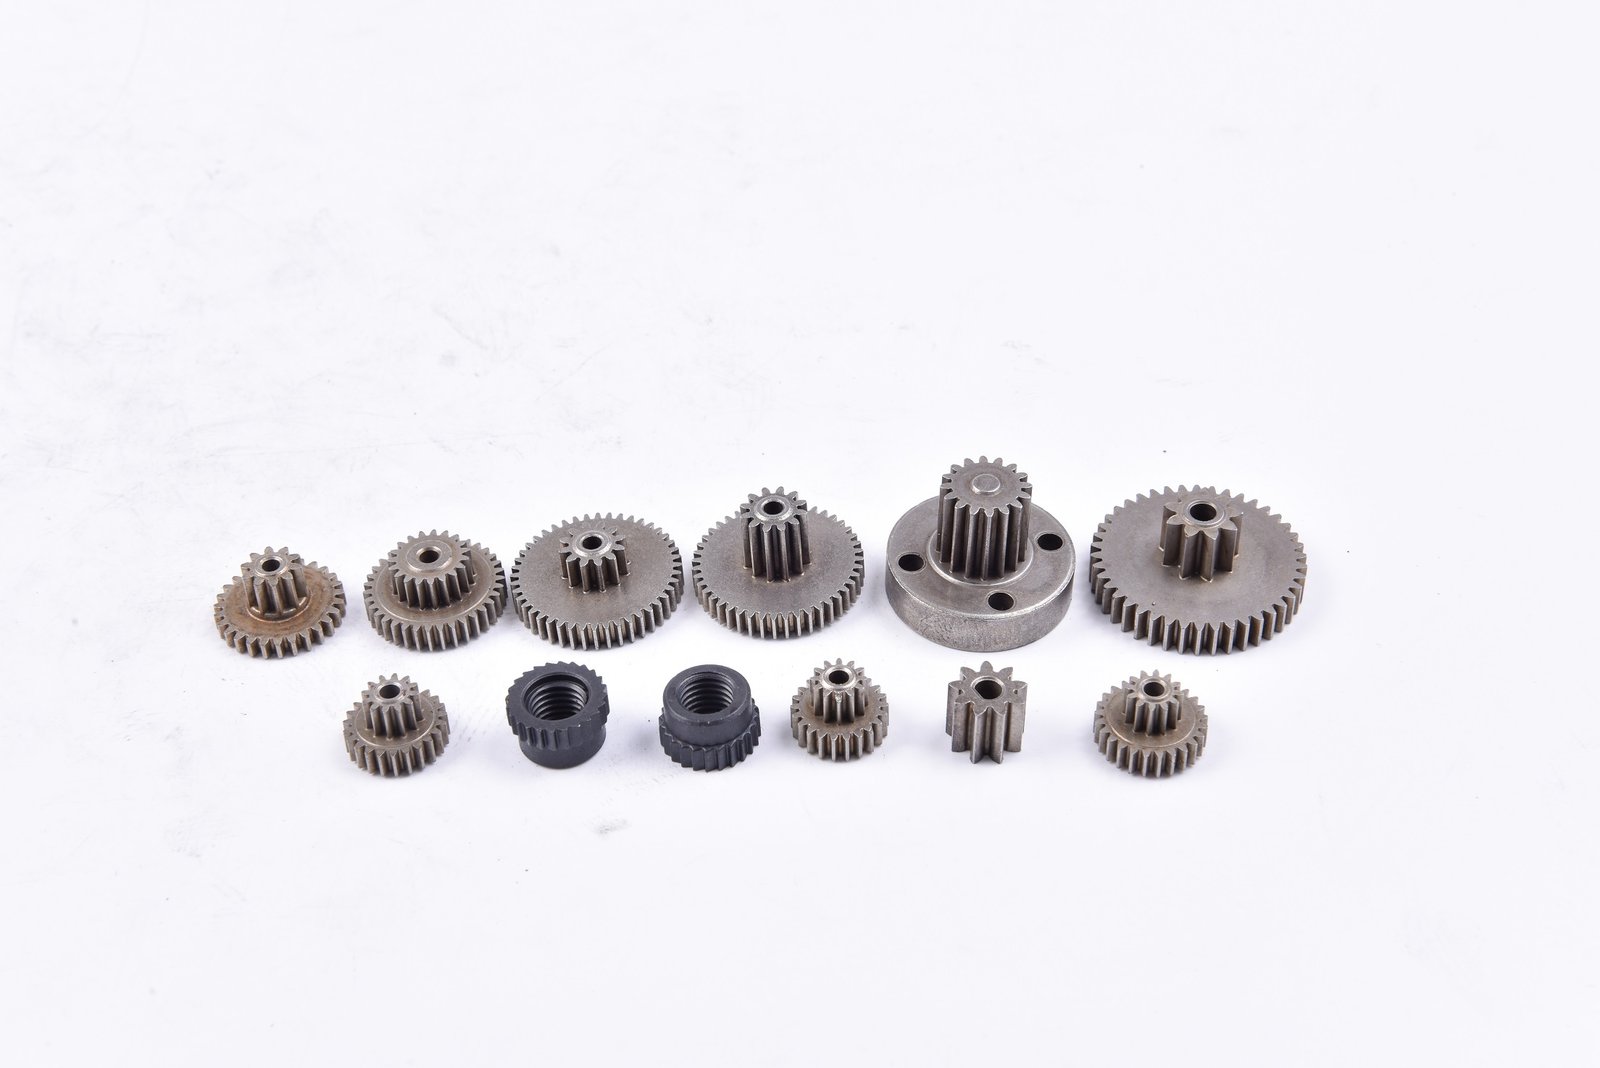
01 · Power & Rotary Tool Gears
Spur and helical gears, pinion shafts, and input/output gears with integrated keyways. Typical 0.4–2.0 kW power tools (impact drivers, hammer drills, rotary hammers). Density 6.8–7.2 g/cm³, surface hardened or through-hardened to fit your duty cycle.
- 01 sintered power tool parts
- 02 PM power tool components
- 03 sintered gear power tool
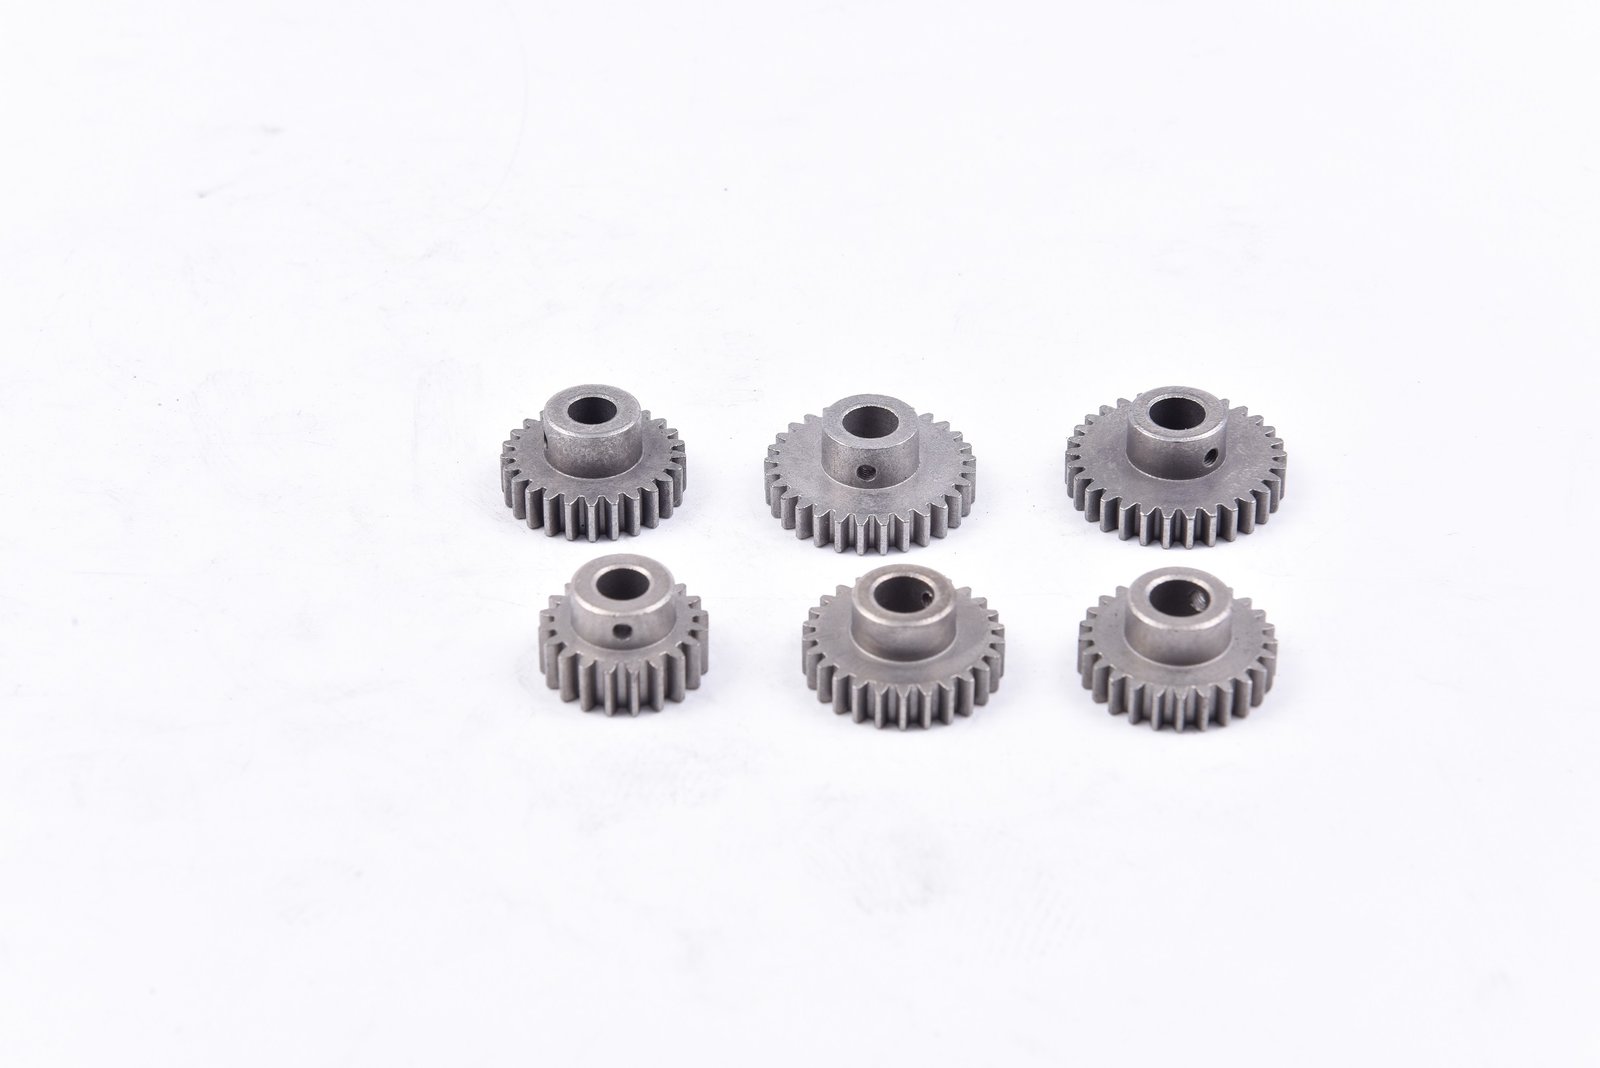
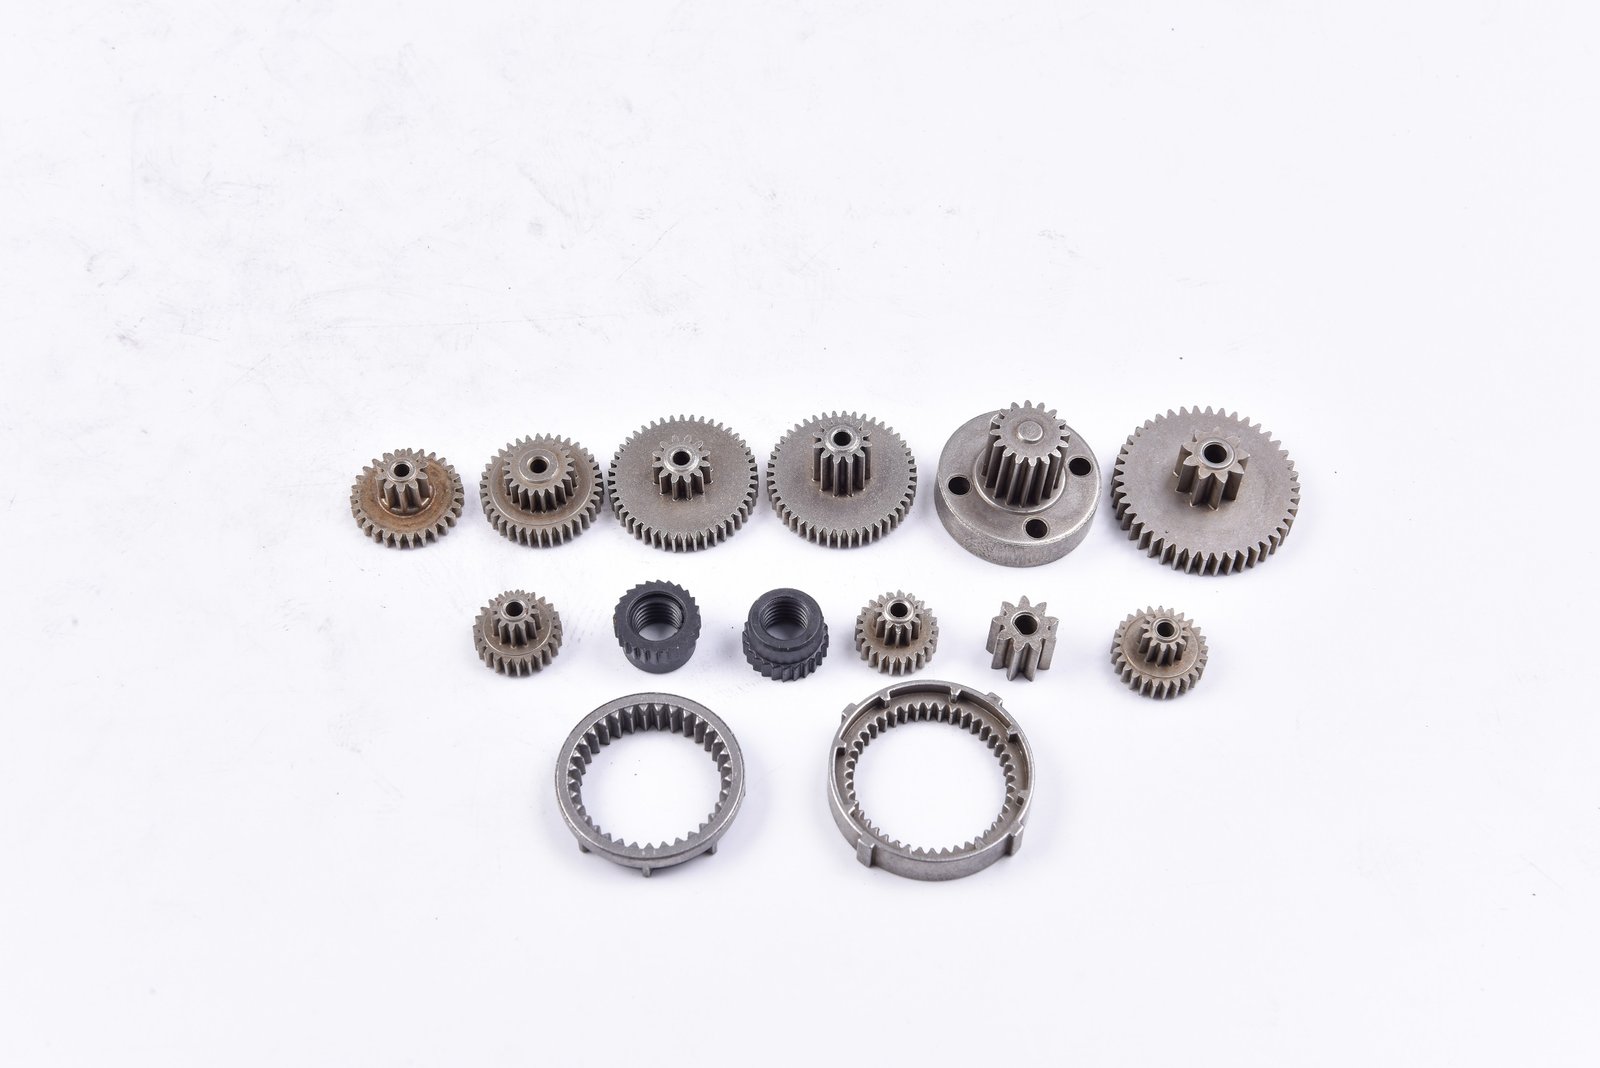
02 · Planetary & Reduction Gears
Planetary gear sets, ring gears, sun and planet pinions, and one-piece carrier/output-shaft assemblies. Built for the 2-stage and 3-stage reductions common in cordless drill and impact-driver gearboxes. Tight concentricity after sizing keeps the planet pinions running true under impact load.
- 04 sintered planetary gear power tool
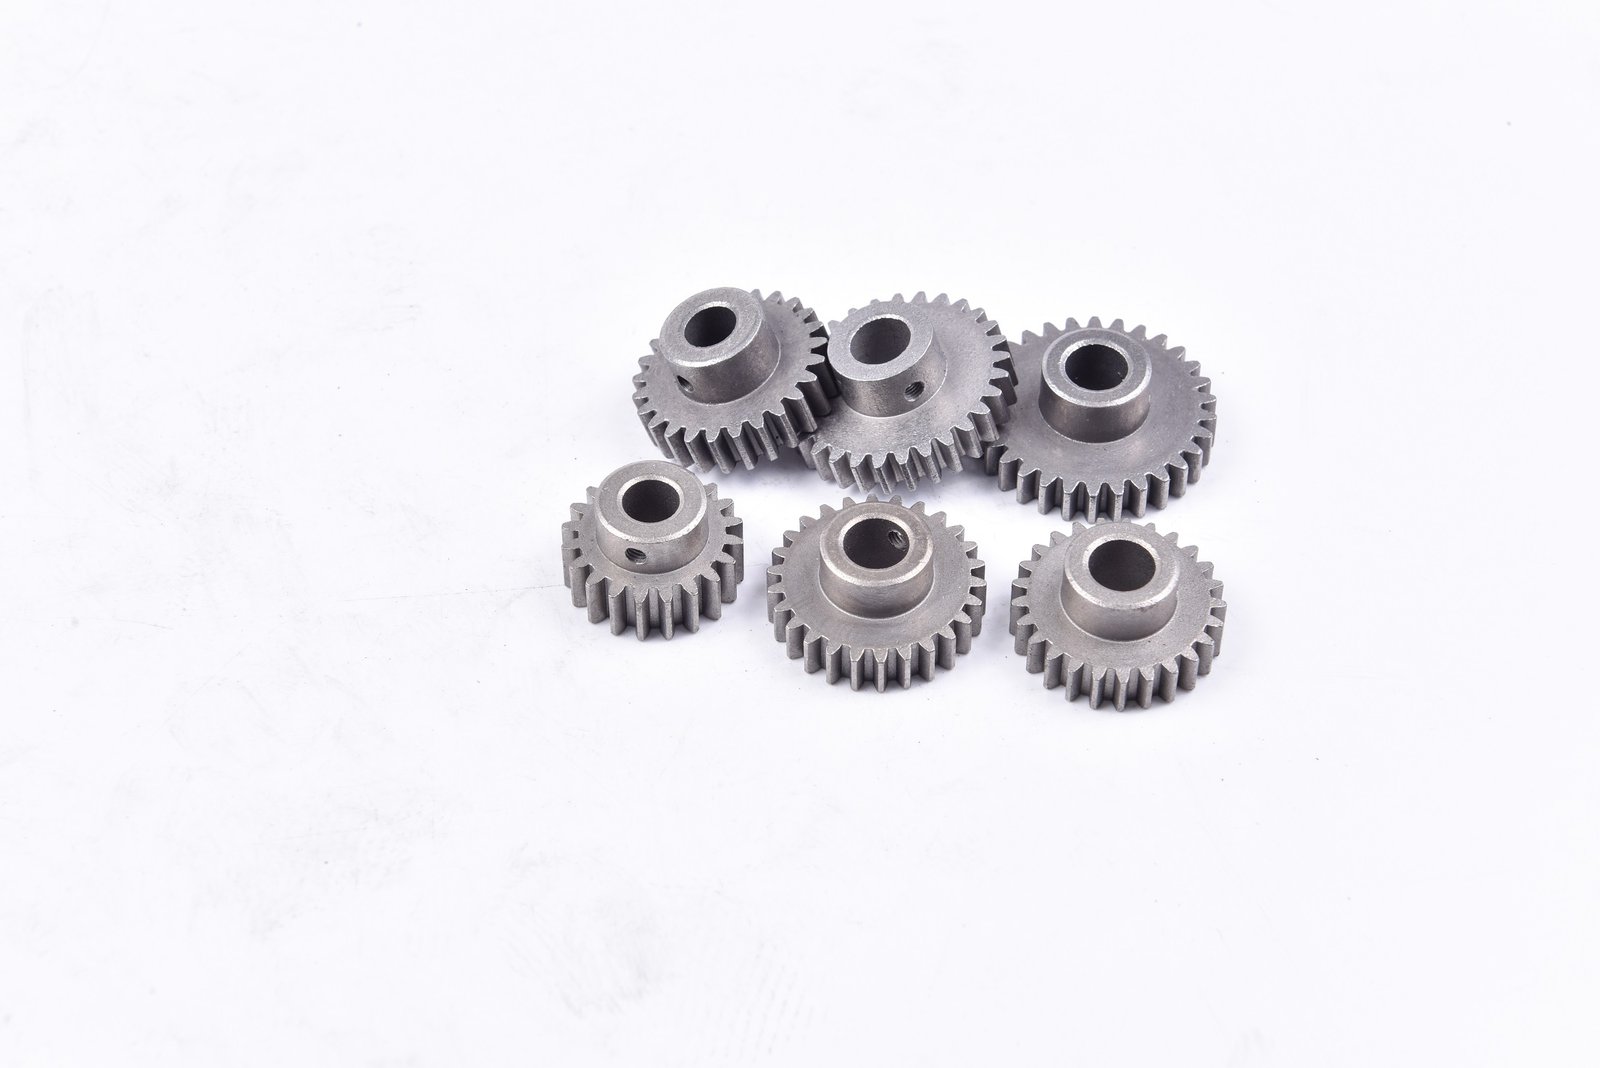
03 · Drill & Driver Pinions
Small helical and spur pinions in matched batches, the parts that take the brunt of impact energy in cordless drills. We press with floating-die tooling to keep tooth profile symmetric, then case-harden where the customer needs it. Dimensional spread within a lot stays inside 0.02 mm on tooth thickness.
- 05 sintered drill gear
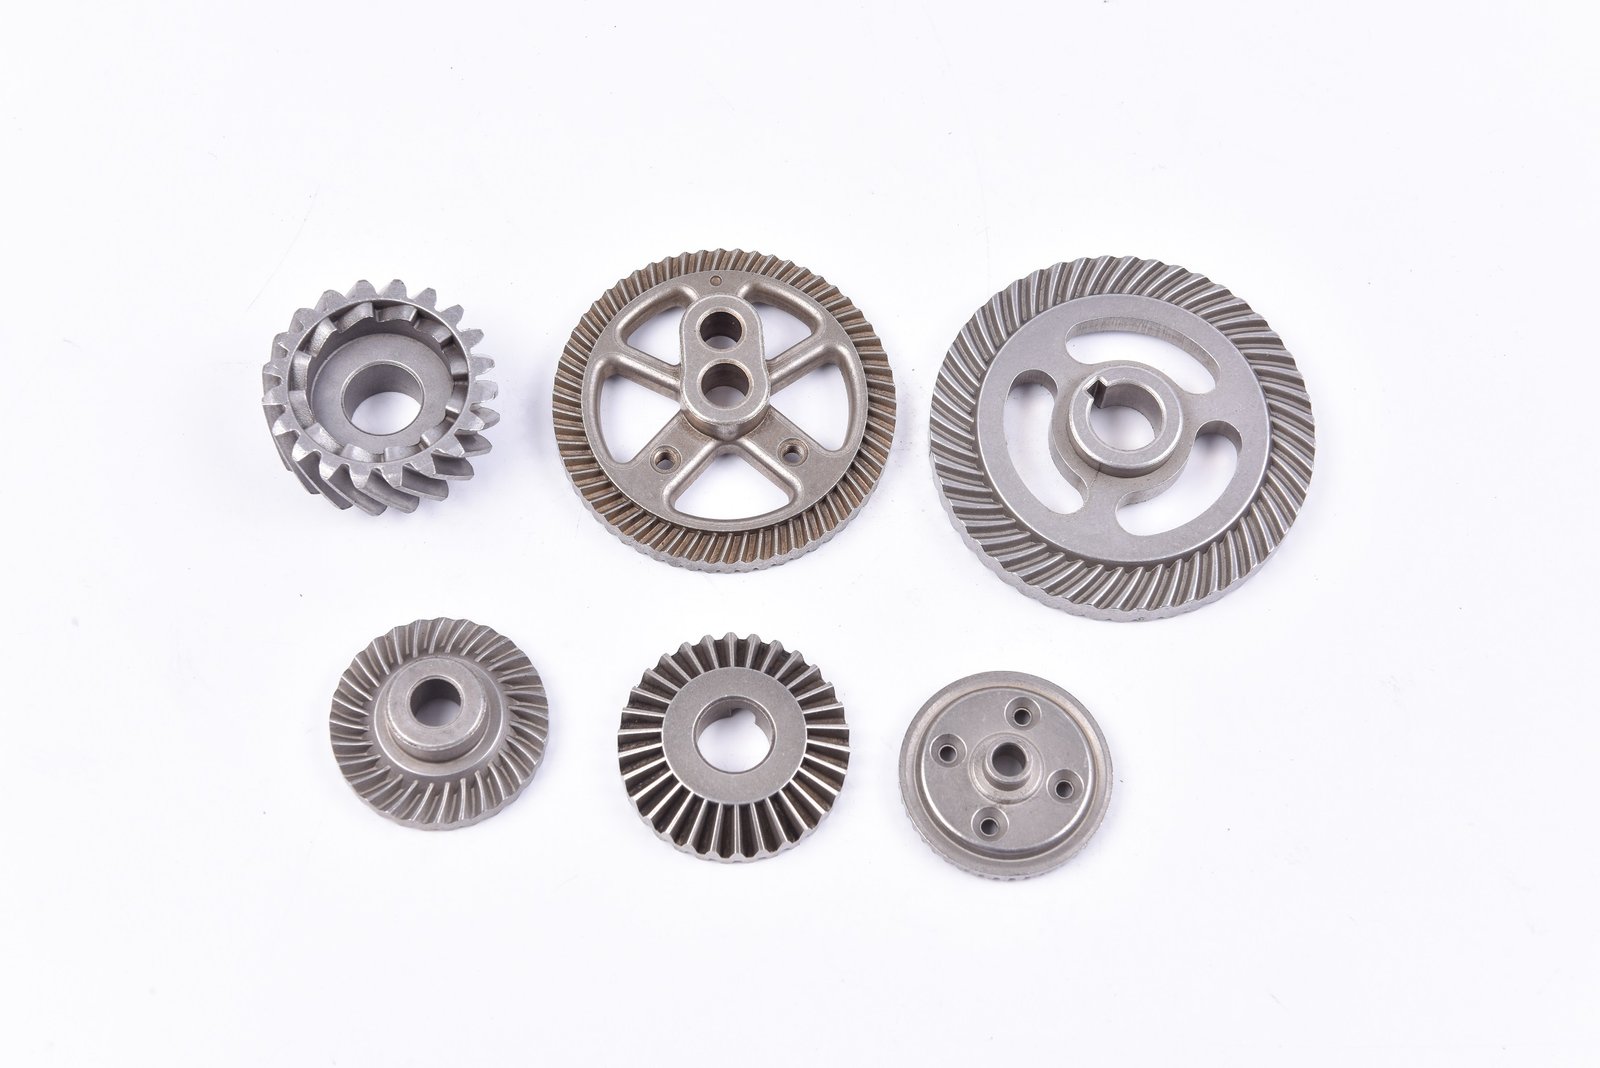
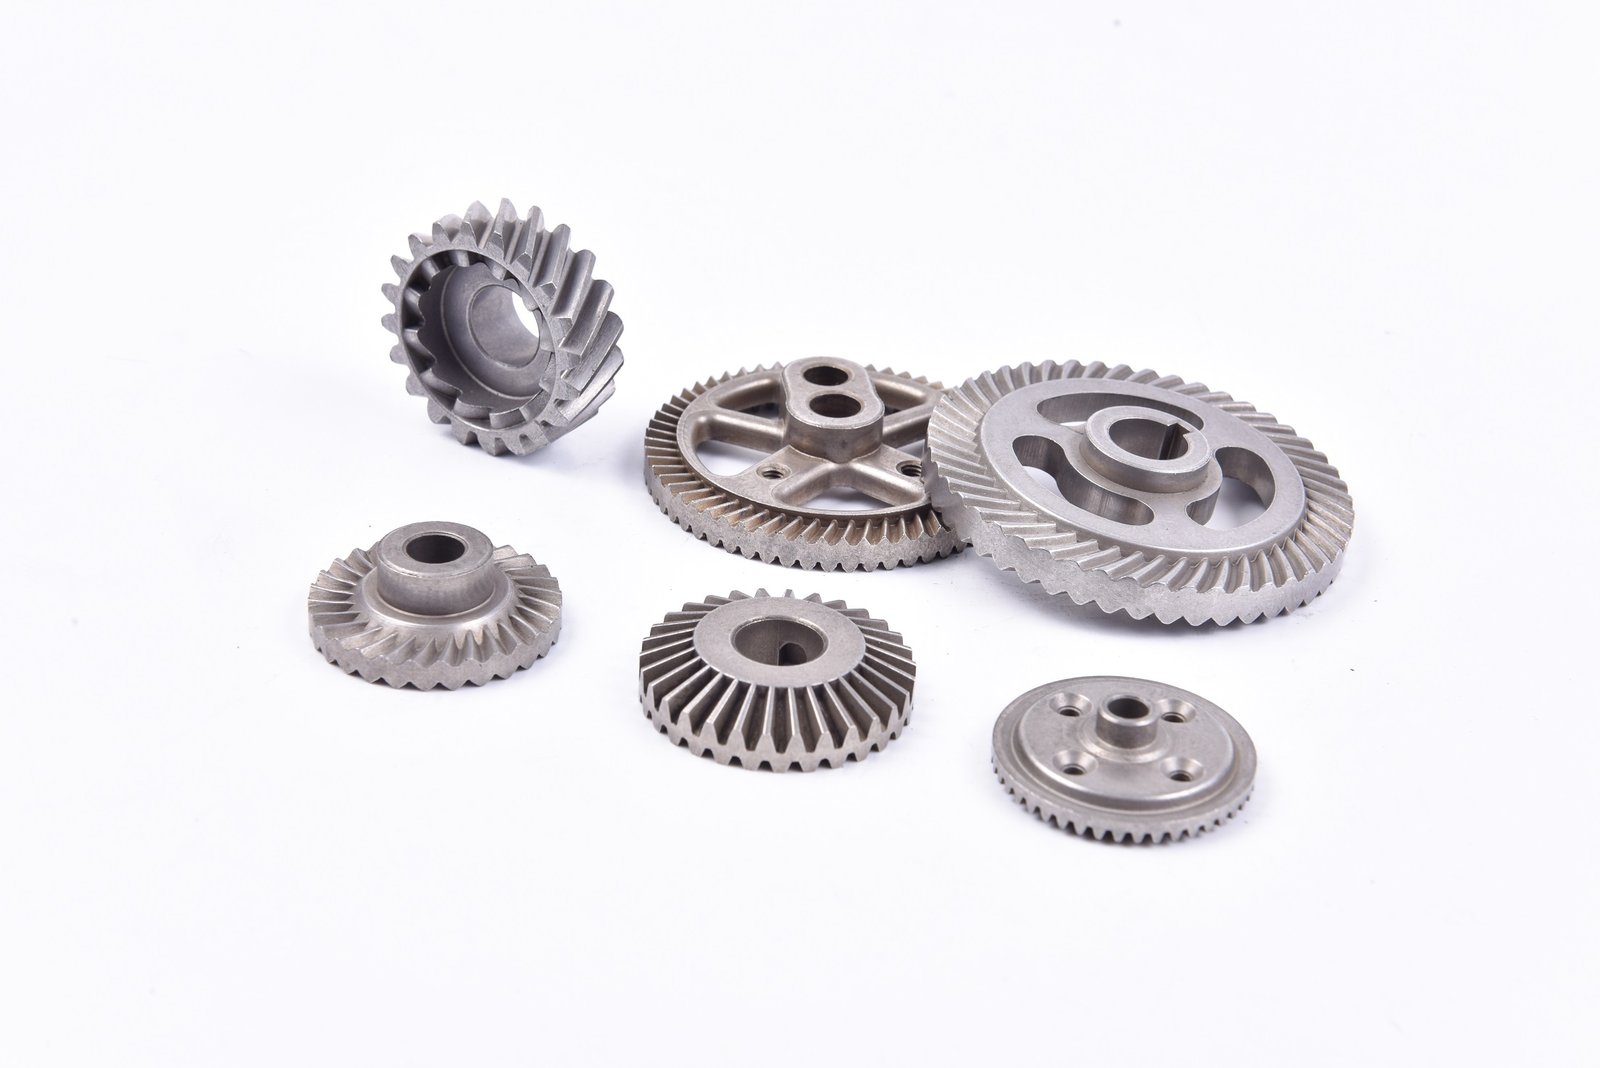
04 · Cutter, Hammer & Grinder Components
Bevel and pinion gears for angle grinders, hammer-clutch dogs, and cutter bodies. These parts run at higher peripheral speed and see shock loading, so we lean on Cu-infiltrated steel and post-sinter HIP where the duty cycle calls for it.
- 06 sintered angle grinder gear
From your 2D drawing to a packed carton in roughly 35 days.
Every step runs inside one factory, so the powder lot, the press, the furnace, and the CMM report all sit on the same batch record.
DFM & Tooling
48 h DFM feedback. Hard tooling T1 around day 20, sample around day 25.
Compaction
19 mechanical and hydraulic presses, 60–800 t. Floating-die where tooth profile symmetry matters.
Sintering
10 continuous-belt and batch furnaces, 1120–1280 °C, endothermic atmosphere.
Sizing & Machining
Re-press for tooth geometry, then CNC finish on bores, keyways, bearing journals.
QA & Packout
Zeiss CMM, gear tester, density check, MPIF 35 material cert, batch-traced carton.
What we hold, what we don’t.
Numbers below are production-typical. We’ll confirm feasibility against your drawing before tooling kicks off.
| Material families | Fe (MPIF F-0000), Ni-steels, Cu-infiltrated steels, 304L/316L stainless variants on request |
|---|---|
| Density | 6.6–7.2 g/cm³ typical (about 85–92% theoretical, MPIF-aligned). Higher on Cu-infiltrated parts. |
| Tensile / hardness | 340–650 MPa UTS as-sintered; up to 45 HRC after heat treat (case or through) |
| Dimensional accuracy | ±0.025 mm on selected critical dimensions after sizing and CNC. Press-direction tolerance wider on green height. |
| Surface finish | As-sintered Ra 2–4 micrometers; after sizing/CNC, Ra 0.8 micrometers on tooth flanks and bearing journals; OD-ground to Ra 0.4 micrometers |
| Gear quality | AGMA Q9–Q10 on application; tested on a Klingelnberg-style gear checker for profile and lead |
| Size envelope | Smallest sintered OD about 8 mm; largest OD roughly 120 mm, limited by press tonnage |
| Annual capacity | 3000+ tons of finished PM parts, including 600+ tons of MIM-grade feedstock capacity |
| Certifications | IATF 16949:2016, ISO 9001:2015, RoHS, REACH, PPAP, IMDS, MPIF 35 material reports |
| MOQ / tooling | 2,000 pcs typical; 10,000+ pcs/year is where PM tooling amortizes cleanly |
Single factory, audited supply chain, honest numbers.
One site, one batch record
Pressing, sintering, sizing, CNC, and final QA all sit on the same factory floor in Ningbo. The MES ties powder lot, press, furnace, and inspection data to every carton, so PPAP submissions and field issues trace back in minutes, not days.
Material data, not marketing
We publish MPIF 35-aligned tensile, hardness, and density curves per grade, not vague “high strength” claims. If a part sits outside the envelope below, we tell you at DFM and propose a MIM or machined-bar fallback.
48-hour DFM, real engineers
Every RFQ gets a written DFM note from a process engineer, not a templated auto-reply. We mark up your drawing with concerns, suggest a tooling split if the geometry is press-unfriendly, and price FAI, PPAP, and ongoing production separately.
Parts we’re running this quarter.
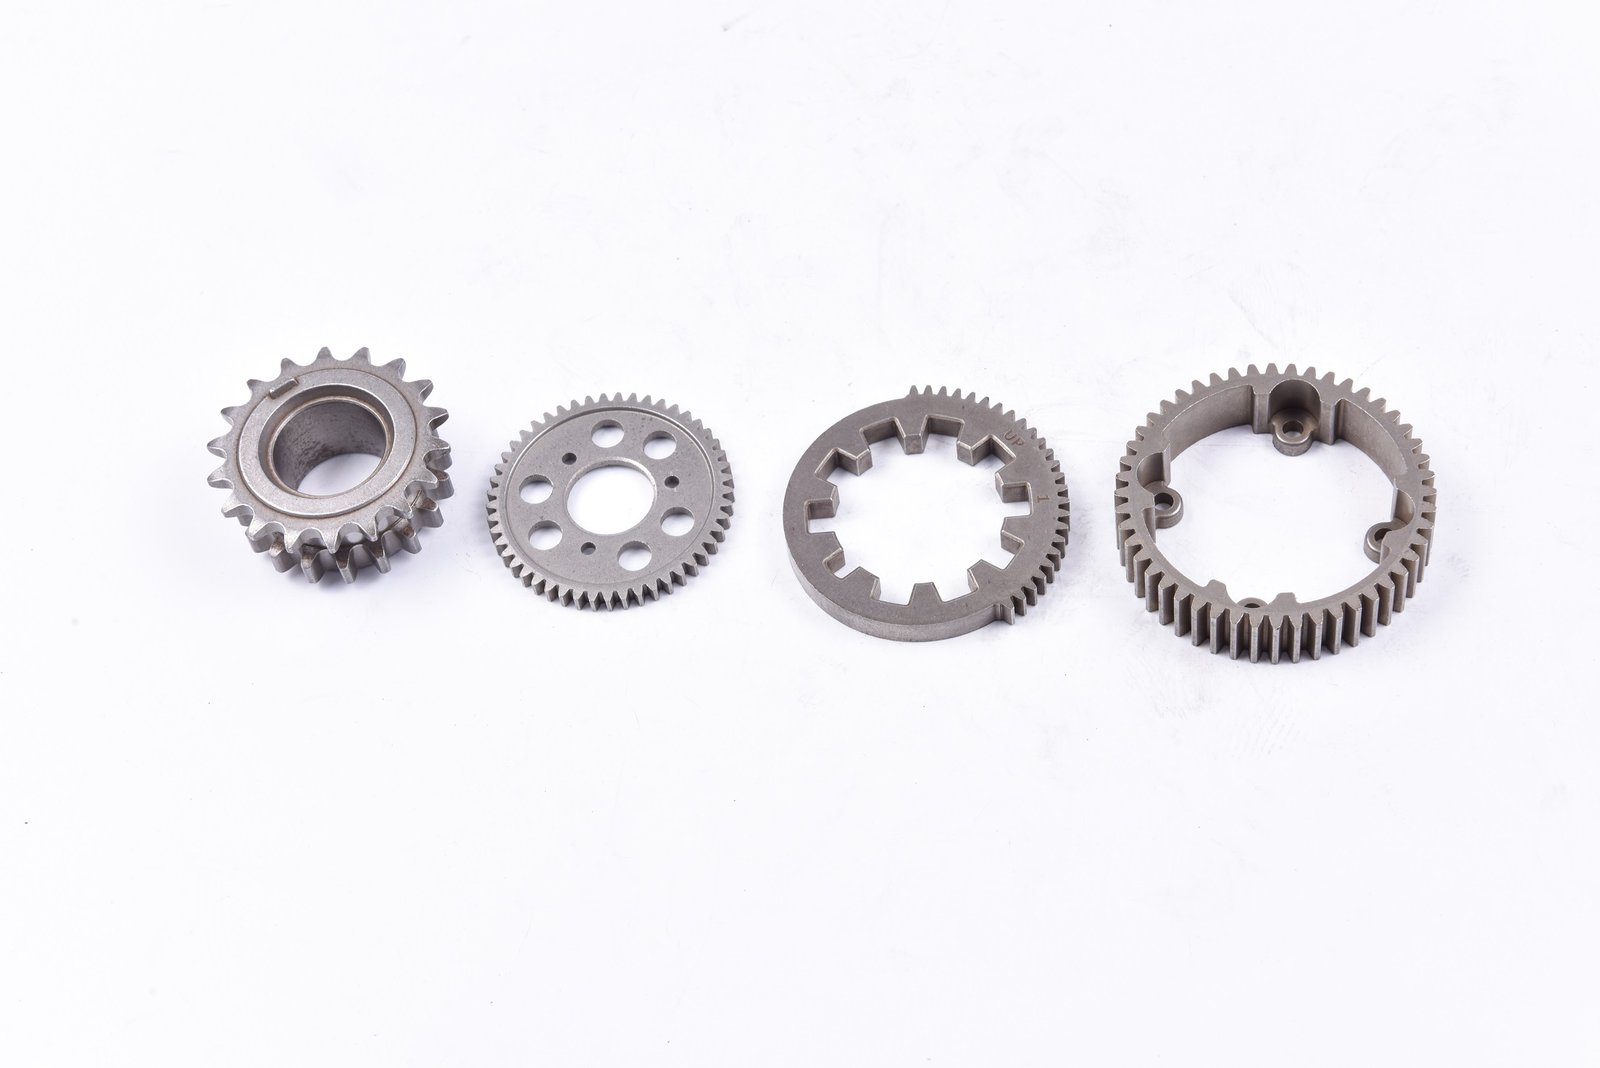
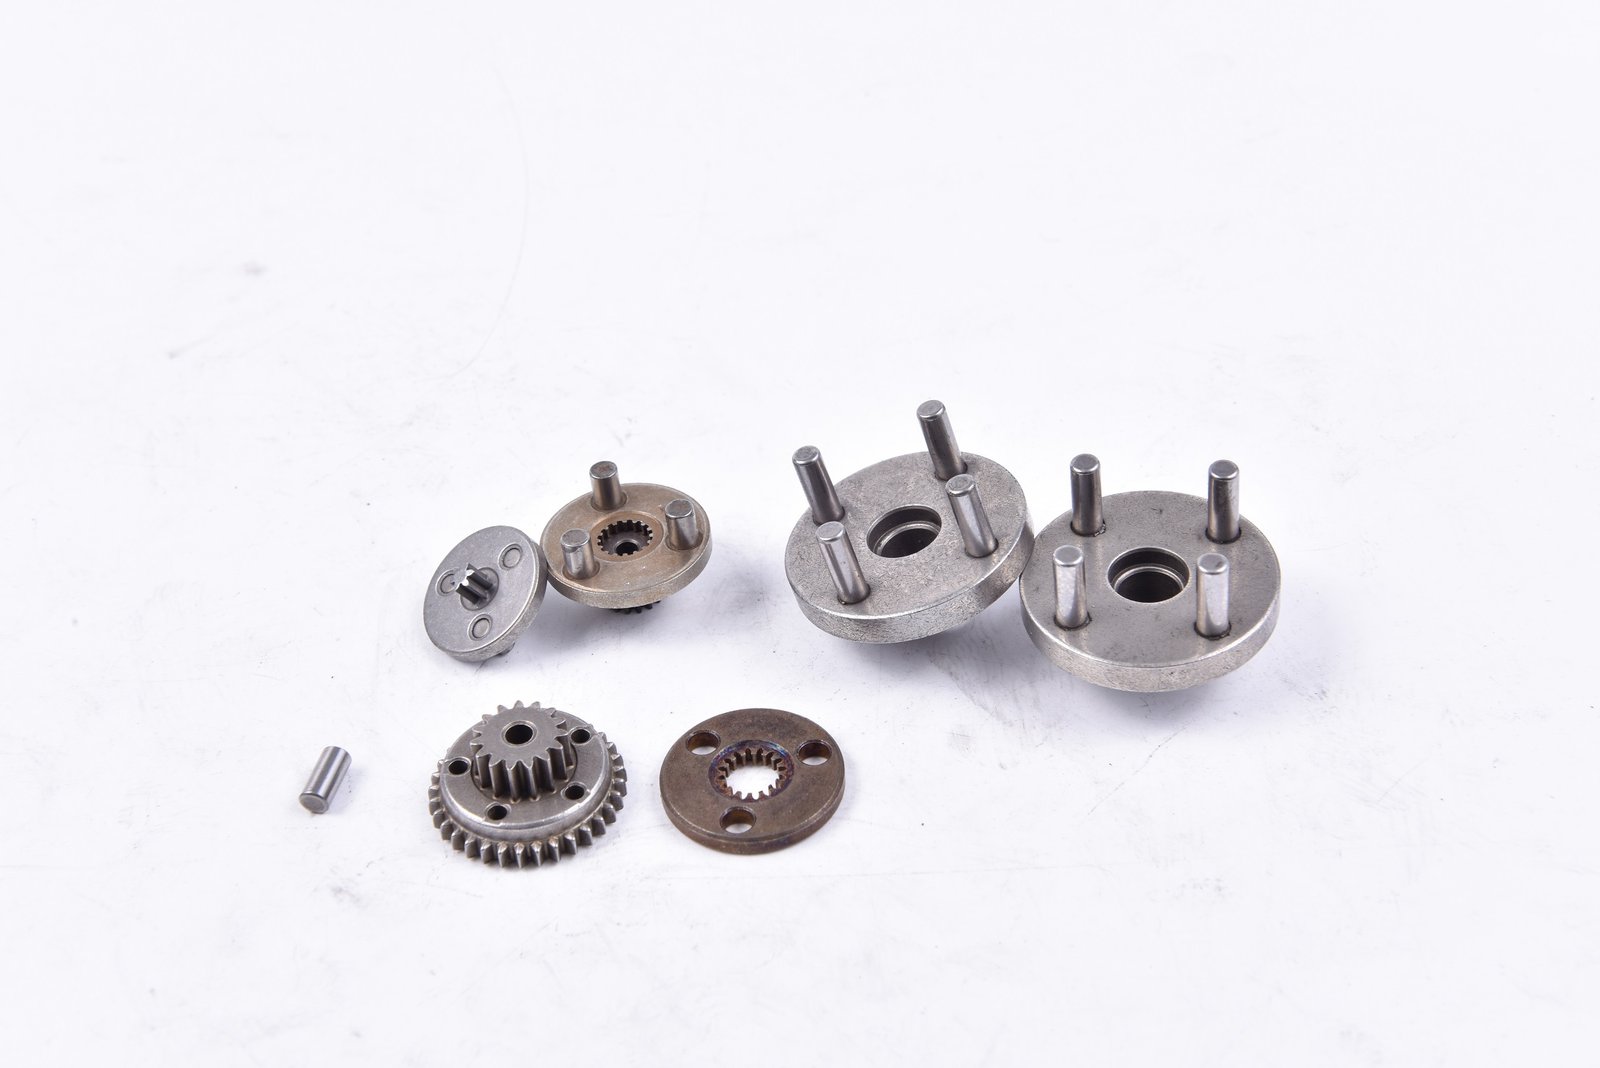
Questions power-tool buyers ask before the first PO.
What surface roughness and post-machining can you hold on sintered power tool gears?
What is the smallest and largest sintered power tool part you can press?
Do you support PPAP for power tool programs?
Can you match a competitor’s part I am already running?
What is the lead time from PO to first production batch?
How do you handle export packaging and documentation for EU/US buyers?
Send your drawing, get a 48-hour DFM.
Tell us the part, the annual volume, and the duty cycle. We’ll come back with a feasibility note, a tooling estimate, and a sample plan within two working days.
Or email info@chinapmfactory.com with your STEP / PDF drawing.
What we make for power tool drivetrains
Grouped by function inside the tool — from main drive gears to clutch and grinder sub-assemblies. Each part is pressed, sintered, sized and finish-machined in our own plant.
Spur & helical gears for power tool drivetrains
Main drive and output gears with keyways, hub bosses and lightening holes. Spur and mixed-pitch helical profiles in one lot, ready for shaft press-fit or heat-treated mating.
- 01sintered power tool parts
- 02PM power tool components
- 03sintered gear power tool

Planetary gear sets and reduction gear stages
Sun, planet and ring-carrier sub-assemblies for planetary reduction gearboxes. Multi-stage combinations for impact drivers, hammer drills and high-torque rotary tools.
- 04sintered planetary gear power tool

Drill pinions and small-module helical gears
Small-module pinions and pinion-idler sets for cordless drills, drivers and rotary hammers. Tight tooth-to-tooth pitch control from lot to lot, so your gear train runs quiet.
- 05sintered drill gear

Angle grinder pinions, hammer clutches and cutter gears
Bevel-helix pinions for angle grinders, hammer clutch plates and sub-assemblies, multi-tooth cutters. Mixed-form gears in the same lot, finish-ground where your drawing requires.
- 06sintered angle grinder gear

How a sintered power tool part leaves our plant
Closed-loop process from your 3D/2D drawing to the shipping carton. DFM feedback at step one, batch-level traceability at step five.
DFM review
48-hour feedback on print feasibility, density, draft, machining stock.
Tooling & sampling
Multi-cavity die, ~20-day lead, first samples within 25 days of PO.
Compacting
19 mechanical and hydraulic presses, 60–800 t, multi-level parts.
Sintering & sizing
10 continuous furnaces; sizing restores critical-dimension geometry.
CNC & inspection
Drilling, broaching, OD/ID grinding; CMM and gear checker reports.
Reading this on a phone? Send your STEP/IGES to info@chinapmfactory.com and we will reply within 48 hours.
Sintered power tool part specifications
Defaults below — we adjust every value to your drawing. Anything outside this range goes to our MIM line or our machine shop.
| Parameter | Typical range · PM process |
|---|---|
| Materials | Fe, Cu-Fe, Fe-Ni, Fe-Cu-Ni-Mo, 316L / 17-4PH stainless on request |
| Density | 6.6–7.2 g/cm³ (about 85–92% of theoretical density) |
| Tensile strength | ~300–700 MPa, material dependent |
| Hardness | As-sintered 40–80 HRB; through-hardened or case-hardened on request |
| Critical-dimension tolerance | ±0.025 mm on selected critical dimensions after sizing & CNC |
| Outer diameter | up to ~120 mm depending on press tonnage and part height |
| Module range | module 0.5–1.5 typical; coarser modules on review |
| Min. order quantity | 2,000 pcs / part number; tooling amortizes economically from 10,000+ pcs/yr |
| Lead time | tooling ~20 days, samples ~25 days after PO, production 30–45 days |
| Quality system | IATF 16949:2016, ISO 9001:2015, PPAP supported |
Density is reported in g/cm³ (line 1) and as a percentage of the material’s theoretical density (line 2) — both are common in PM datasheets; convert as 1 g/cm³ = 1000 kg/m³.
Three reasons buyers keep re-issuing POs
Not a marketing claim — each point is something our customers can audit on a sample shipment or a supplier audit visit.
Press to sinter under one roof
Compacting, sintering, sizing and finish-machining are all on the same campus in Ningbo. No subcontracted steps between die and dispatch — one quality system, one batch lot, one MES record.
Pitch and density you can re-run
Lot-level records of sintered density, hardness and gear pitch. Re-orders open the same MES batch, so a 2027 PO can match a 2025 sample to within your drawing tolerance.
DFM in 48 hours, even when the answer is no
If a part shouldn’t be PM, we say so and route it to our MIM or machining lines. If it should be PM but your print is over-specified, we tell you which tolerance to relax and why.
Lot photos, not renderings
Real production lots leaving our QA area. If you would like a photo of a specific lot before shipment, request it on your PO and we will attach it to the MTC.


Questions we get from power tool buyers
What surface roughness and post-machining can you hold on sintered power tool gears?
Can you make stainless (316L / 17-4PH) power tool parts on the PM line?
What is the smallest and largest sintered power tool part you can press?
Do you support PPAP and IMDS for power tool programs?
What is the typical MOQ and how does it relate to tooling amortization?
Can you ship RoHS, REACH and PPWR-compliant power tool parts to the EU?
Need a sintered power tool part quoted?
Send us your STEP / IGES / PDF, the annual forecast and the critical-dimension notes. We will reply with a DFM review, a piece price range, and tooling lead time within 48 hours.
DFM in 48h · tooling ~20 days · samples ~25 days · MOQ 2,000 pcs