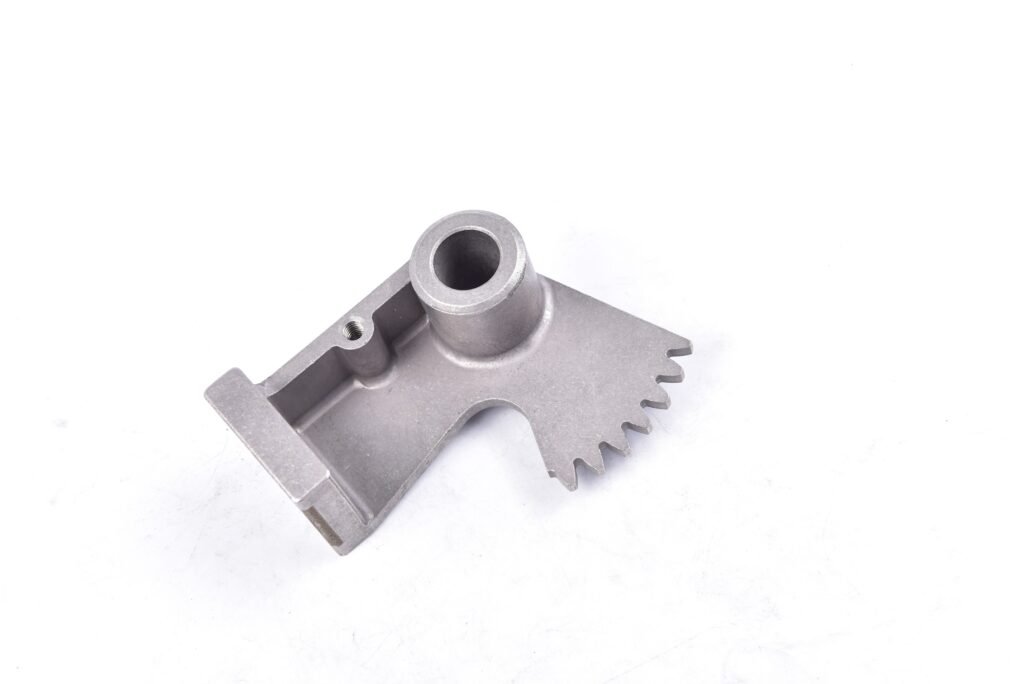
Stainless Steel PM Parts: Materials, Properties, Applications & Manufacturing
A practical engineering guide to stainless steel powder metallurgy — grade selection, achievable mechanical properties, corrosion performance, tolerances and the manufacturing controls that separate a reliable stainless steel PM manufacturer from an ordinary sintered parts supplier.
Stainless steel PM (powder metallurgy) is a net-shape process that compacts water-atomized stainless steel powders at 400–800 MPa and sinters them at 1,120–1,350 °C in hydrogen, nitrogen or vacuum atmospheres. Sintered stainless steel components typically deliver 6.4–7.4 g/cm³ density and 200–650 MPa tensile strength (up to ~1,100 MPa for aged 17-4PH) with controlled porosity and ±0.05–0.1 mm as-sintered tolerances. JH PM produces stainless steel PM parts from 2,000+ pcs per batch, making it the lowest-cost route for corrosion-resistant, complex geometry at volume.
Quick Summary (Key Engineering Data)
- Material coverage: SS-304, SS-304L, SS-316, SS-316L, SS-410, SS-420, SS-434, SS-430N2 and 17-4PH per MPIF Standard 35.
- Mechanical envelope: tensile strength from ~200 MPa (ferritic, as-sintered) to ~650 MPa (austenitic) and ~1,100 MPa (aged 17-4PH); density 6.4–7.4 g/cm³.
- Primary applications: automotive exhaust & fluid systems, medical instruments, marine hardware, food equipment, fluid control valves.
- JH PM capabilities: 19 PM presses (6–1,000 tons), 2 continuous sintering lines with hydrogen/nitrogen atmospheres, 3 ZEISS CMMs, 25-day tooling, 35-day T0 samples, 2,000 pcs MOQ.
What Is Stainless Steel PM?
Stainless steel powder metallurgy is a net-shape manufacturing process in which fine, water-atomized stainless steel powders are blended with lubricant, compacted into a precision die at 400–800 MPa, and sintered at approximately 1,120–1,350 °C. Because stainless powder surfaces carry a persistent chromium oxide layer, sintering must take place in a controlled hydrogen, vacuum or nitrogen-based atmosphere to reduce that oxide so particles metallurgically bond into a strong, corrosion-resistant part. The result is stainless steel sintered parts with near casting-level density, controlled porosity and zero machining scrap.
JH PM works across the three main stainless powder systems:
- Austenitic 300 series (SS-304 / SS-316): non-magnetic, weldable, and offering the best corrosion resistance — the default for medical, food and marine exposure.
- Ferritic / martensitic 400 series (SS-410 / SS-420 / SS-434): magnetic, hardenable and lower cost — the workhorses of automotive exhaust and fluid systems.
- Precipitation-hardening 17-4PH: the highest-strength stainless steel PM material, reaching up to ~1,100 MPa tensile strength after solution treatment and aging.
- Nitrogen-alloyed ferritics (SS-430N2): nitrogen uptake during sintering raises strength and pitting resistance at low cost.
Stainless Steel PM Materials Family
Selecting the right stainless steel PM material is a balance of corrosion environment, strength requirement and cost. The table below summarizes the standard grades we press and sinter, per MPIF Standard 35 nomenclature.
| Material Family | Standard Grade / Typical Composition | Typical Properties | Primary Applications |
|---|---|---|---|
| Austenitic | SS-304 / SS-304L (18% Cr, 8–12% Ni) | Excellent corrosion resistance, non-magnetic, weldable | Food equipment, medical devices, fluid fittings |
| Austenitic | SS-316 / SS-316L (16–18% Cr, 10–14% Ni, 2–3% Mo) | Superior pitting, crevice and chloride corrosion resistance | Marine hardware, medical instruments, chemical processing |
| Ferritic | SS-410 / SS-410L (11.5–13.5% Cr) | Magnetic, moderate corrosion resistance, economical | Automotive exhaust parts, brackets, sensor fittings |
| Martensitic | SS-420 (12–14% Cr, higher carbon) | Hardenable to ~HRC 45–50, excellent wear resistance | Cutting tools, pump vanes, valve components |
| Ferritic | SS-434 (16–18% Cr, 0.75–1.25% Mo) | Added Mo improves salt-spray corrosion resistance | Automotive exterior trim fasteners, exhaust systems |
| Nitrogen-alloyed Ferritic | SS-430N2 (17% Cr with N alloying) | Sinter-hardening nitrogen uptake gives higher strength | High-strength magnetic components, structural brackets |
| Precipitation-Hardening | 17-4PH (17% Cr, 4% Ni, 3–5% Cu) | ~1,100 MPa tensile strength after precipitation aging | Aerospace, high-stress structural components |
Properties of Stainless Steel PM Parts
Stainless steel powder metallurgy properties are governed by grade, sintered density and atmosphere control. These are the six property areas design engineers should evaluate when specifying stainless steel PM parts.
Density & Porosity
Typical sintered densities range from 6.4 to 7.4 g/cm³. Porosity can be left controlled for self-lubrication or filtration, or densified (sizing, re-press, HIP) to maximize corrosion resistance and strength.
Corrosion Resistance
Performance depends on density and sintering atmosphere: hydrogen vs. nitrogen alters chromium distribution at particle boundaries. Properly sintered 316L stainless steel PM parts pass ASTM B117 salt-spray testing.
Tensile & Yield Strength
Strength ranges from ~200 MPa for ferritic grades as-sintered to ~650 MPa for austenitic grades, and up to ~1,100 MPa for aged 17-4PH — comparable to many cast stainless alloys at volume.
Apparent Hardness
As-sintered parts typically measure HRB 40–90. Martensitic SS-420 can be quench-and-temper hardened to HRC 45–50 for wear-critical pump and tooling components.
Machinability
303-type powders with sulfur additions improve chip formation. Resin impregnation seals surface pores, extending tool life and delivering a cleaner machined finish on stainless steel PM parts.
Dimensional Stability
Sintering shrinkage of stainless steel is higher than iron-based PM: expect ±0.05–0.1 mm as-sintered and ±0.025 mm with sizing. Tight atmosphere control is essential for lot-to-lot consistency.
Stainless Steel PM Parts: Common Applications
Stainless steel sintered parts applications concentrate wherever corrosion resistance, moderate loads and complex geometry converge at volume.
Automotive & Exhaust
Oxygen sensor fittings, EGR valve components, fuel system filter elements and brake hardware sintered in ferritic SS-410 and SS-434.
Medical & Surgical
Surgical instrument components, orthodontic parts and drug delivery pump components in non-magnetic, biocompatible 316L.
Food, Beverage & Chemical Processing
Spray nozzles, valve seats, pump components and mixer bearings in austenitic 304/316L for washdown and chemical environments.
Marine & Outdoor Hardware
Corrosion-resistant latch bodies, deck hardware and fastener bodies in molybdenum-bearing 316L and 434 grades.
Fluid & Pneumatic Control
Flow restrictors, porous mufflers and silencers, filter discs and valve stems leveraging controlled porosity.
Household & Power Tools
Gear components, corrosion-resistant housings, washers and spacers combining strength with aesthetic corrosion resistance.
Why Use Stainless Steel PM Instead of Casting or Machining?
For stainless steel sintered parts, the economics are decided by geometry complexity and volume. This comparison shows where stainless steel PM wins — and where casting or machining remains the better route.
| Factor | Stainless Steel PM | Cast / Machined Stainless |
|---|---|---|
| Material Utilization | >95% — powder goes into the part, no gates or runners | Casting runners/gates plus machining scrap can waste 30–50% of alloy |
| Surface Finish & Consistency | As-sintered fine finish; highly repeatable lot-to-lot | Casting surface varies with process; machining adds cycle time |
| Integrated Geometry | Multi-level flanges, splines and gear teeth molded in one press stroke | Features must be machined at significant added cost |
| Porosity Control | Controllable — self-lubricating or filtration function by design | Casting must be pore-free; porosity is a defect, not a feature |
| Corrosion Performance | Oxide-reducing atmosphere yields clean grain boundaries | Cast segregation and sigma-phase risk degrade corrosion resistance |
| Tooling vs Unit Cost | Dedicated tooling; lowest unit cost above 2,000–10,000+ pcs | Low tooling cost but high per-piece machining time |
Engineering Insight: When to Pick Stainless PM vs. Casting/Machining
Stainless steel powder metallurgy is the ideal choice for small-to-medium complex parts produced at 2,000+ volume that need corrosion resistance without the cost of machining from bar stock. Investment casting or machining wins for very low volumes, very large parts, or pressure-tight vessels that require HIP or full impregnation — talk to our engineers before finalizing the route.
Stainless Steel PM Manufacturing Process
Producing consistent sintered stainless steel components requires atmosphere and thermal discipline at every step. Here is how JH PM manufactures stainless steel PM parts, from powder to packed goods.
Powder Selection & Blending
Water-atomized 300/400 series powders are blended with a lubricant that must burn off completely, leaving no carbon residue that would degrade corrosion resistance.
Die Compaction
Powder is pressed at 400–800 MPa into a green part with the full net geometry — multi-level, splined or gear-toothed — ready for the furnace.
De-lubrication & Sintering
A slow burn-off zone prevents carbon pickup, then parts sinter at 1,120–1,350 °C in hydrogen, vacuum or nitrogen-based atmosphere. Hydrogen reduces the chromium oxide film, enabling interparticle neck formation.
Secondary Operations
Sizing and coining tighten tolerances to ±0.025 mm; CNC machining adds features; oil or resin impregnation seals porosity where needed.
Heat Treatment / Sinter-Hardening
Solution plus precipitation aging for 17-4PH, quench-and-temper for SS-420, and nitrogen-uptake sinter-hardening for ferritic grades.
Quality Inspection & Packing
Density to ASTM B962, corrosion/salt-spray testing, ZEISS CMM inspection, passivation and traceable packing for every stainless steel PM lot.
Want the fundamentals first? Read our Powder Metallurgy Sintering Process guide or our PM Tolerances Capabilities overview.
Stainless Steel PM Tolerances & Quality Control
Stainless steel powder metallurgy tolerances are tighter than most engineers expect, but they depend on strict control of powder lots, sintering temperature and atmosphere. Our QC plan for stainless steel sintered parts:
| Inspection Parameter | Standard Test Method | Target Control Range / Benchmark |
|---|---|---|
| Density Verification | ASTM B962 (Archimedes) | 6.40–7.40 g/cm³; lot tolerance ±0.05 g/cm³ |
| Dimensional Integrity | ZEISS 3D CMM / Optical Comparator | ±0.05–0.1 mm as-sintered; ±0.025 mm after sizing |
| Apparent Hardness | ASTM E18 (Rockwell) | HRB 40–90 as-sintered; HRC 45–50 heat treated |
| Corrosion Resistance | ASTM B117 salt spray / ASTM G48 | Verifies passivation and pitting resistance on 316L lots |
| Microstructure Analysis | Metallographic cross-section | Pore morphology, grain size, interparticle necking, carbide precipitation check |
| Lot Traceability | ISO / IATF 16949 systems | 100% powder lot, furnace run and press batch logging |
For the full metrology framework, see our Powder Metallurgy Quality Control & Metrology Guide.
Why Source Stainless Steel PM Parts from JH PM?
19 PM Compaction Presses
Press capacities from 6 to 1,000 tons cover tiny medical fittings to large automotive structural stainless steel PM parts.
Continuous Sintering Furnaces
Hydrogen, nitrogen and vacuum-capable lines with zone monitoring — critical for chromium oxide reduction and consistent corrosion performance.
In-House ZEISS CMM Metrology
3 ZEISS CMMs, optical projectors and metallographic preparation keep stainless steel PM tolerances verifiable on every lot.
Corrosion Testing + Rapid DFM & Tooling
In-house salt-spray testing, MPIF grade guidance, 25-day tooling and 35-day T0 samples accelerate your stainless steel PM program.
Flexible MOQ
2,000 pcs MOQ supports pilot runs and scales seamlessly to million-piece annual programs.
IATF 16949 Certified Quality
PPAP Level 3 documentation and low-PPM delivery performance trusted by automotive and medical OEM supply chains.
Frequently Asked Questions
What is stainless steel PM?
Stainless steel PM (powder metallurgy) is a net-shape manufacturing process in which water-atomized stainless steel powders are compacted in a die at 400–800 MPa and sintered at 1,120–1,350 °C in a controlled hydrogen, nitrogen or vacuum atmosphere. The reducing atmosphere removes the chromium oxide layer from powder surfaces so particles metallurgically bond, producing stainless steel sintered parts with 6.4–7.4 g/cm³ density and controlled porosity without machining waste.
What materials are used in stainless steel PM?
Common stainless steel PM materials include austenitic SS-304, SS-304L, SS-316 and SS-316L; ferritic and martensitic SS-410, SS-420, SS-434 and nitrogen-alloyed SS-430N2; and precipitation-hardening 17-4PH. Grade designations and property envelopes follow MPIF Standard 35.
What are stainless steel PM parts used for?
Typical stainless steel sintered parts applications include automotive exhaust and fuel system components, surgical and medical instrument parts, marine hardware, food processing spray nozzles and valve seats, fluid control valves, and porous filters, mufflers and silencers.
Is stainless steel PM corrosion resistant?
Yes, when properly sintered. Corrosion resistance depends on sintered density and atmosphere control: hydrogen sintering reduces the chromium oxide film and yields clean grain boundaries, while nitrogen atmospheres can alter chromium distribution. Properly sintered 316L stainless steel PM parts pass salt-spray (ASTM B117) testing.
How strong are stainless steel PM parts?
As-sintered stainless steel PM parts typically achieve tensile strengths of about 200–650 MPa depending on grade and density. Heat-treated 17-4PH can reach approximately 1,100 MPa, and hardened SS-420 achieves apparent hardness of HRC 45–50.
What is the difference between stainless steel PM and investment casting?
Stainless steel PM is a near-net process with material utilization above 95 percent, molded-in features such as splines and multi-level flanges, and consistent lot-to-lot repeatability. Investment casting requires gates and runners, generates machining scrap, and typically needs secondary operations to hold tight features.
Can stainless steel PM parts be made pressure-tight?
Yes. The residual porosity of stainless steel powder metallurgy parts can be sealed by resin or copper impregnation, or eliminated by hot isostatic pressing (HIP), making sintered stainless steel components suitable for pressure-tight and leak-resistant applications.
What production volume is suitable for stainless steel PM?
Stainless steel PM becomes cost-effective above roughly 2,000 pcs per batch, with the lowest unit cost typically achieved at 10,000 to 1,000,000+ pieces annually, where dedicated tooling investment is fully amortized.
Ready to Optimize Your Stainless Steel PM Component Design?
Send us your 2D PDF drawings or 3D STEP models along with your target annual volume, service environment (chloride, marine or food-grade exposure) and material preference. Our engineering team will return DFM feedback and a quote within 48 hours.
Upload Drawing for DFM Review