Sintered Textile Machinery Parts
Sintered PM parts for weaving, spinning, knitting and dyeing machines. Gears, oil-impregnated bushings, timing pulleys, cams and structural parts made in our IATF 16949 factory in Ningbo. In-house PM line, 16 presses, 10 sintering furnaces, 3 Zeiss CMMs.
Common fitments: Toyota JAT810, Tsudakoma, Picanol Optimax / GTM, Itema R9500, Sulzer G6200, Somet Thema, plus generic rapier / projectile / air-jet / water-jet looms. 20-day tooling, 25-day first-article samples, 48 h DFM review.
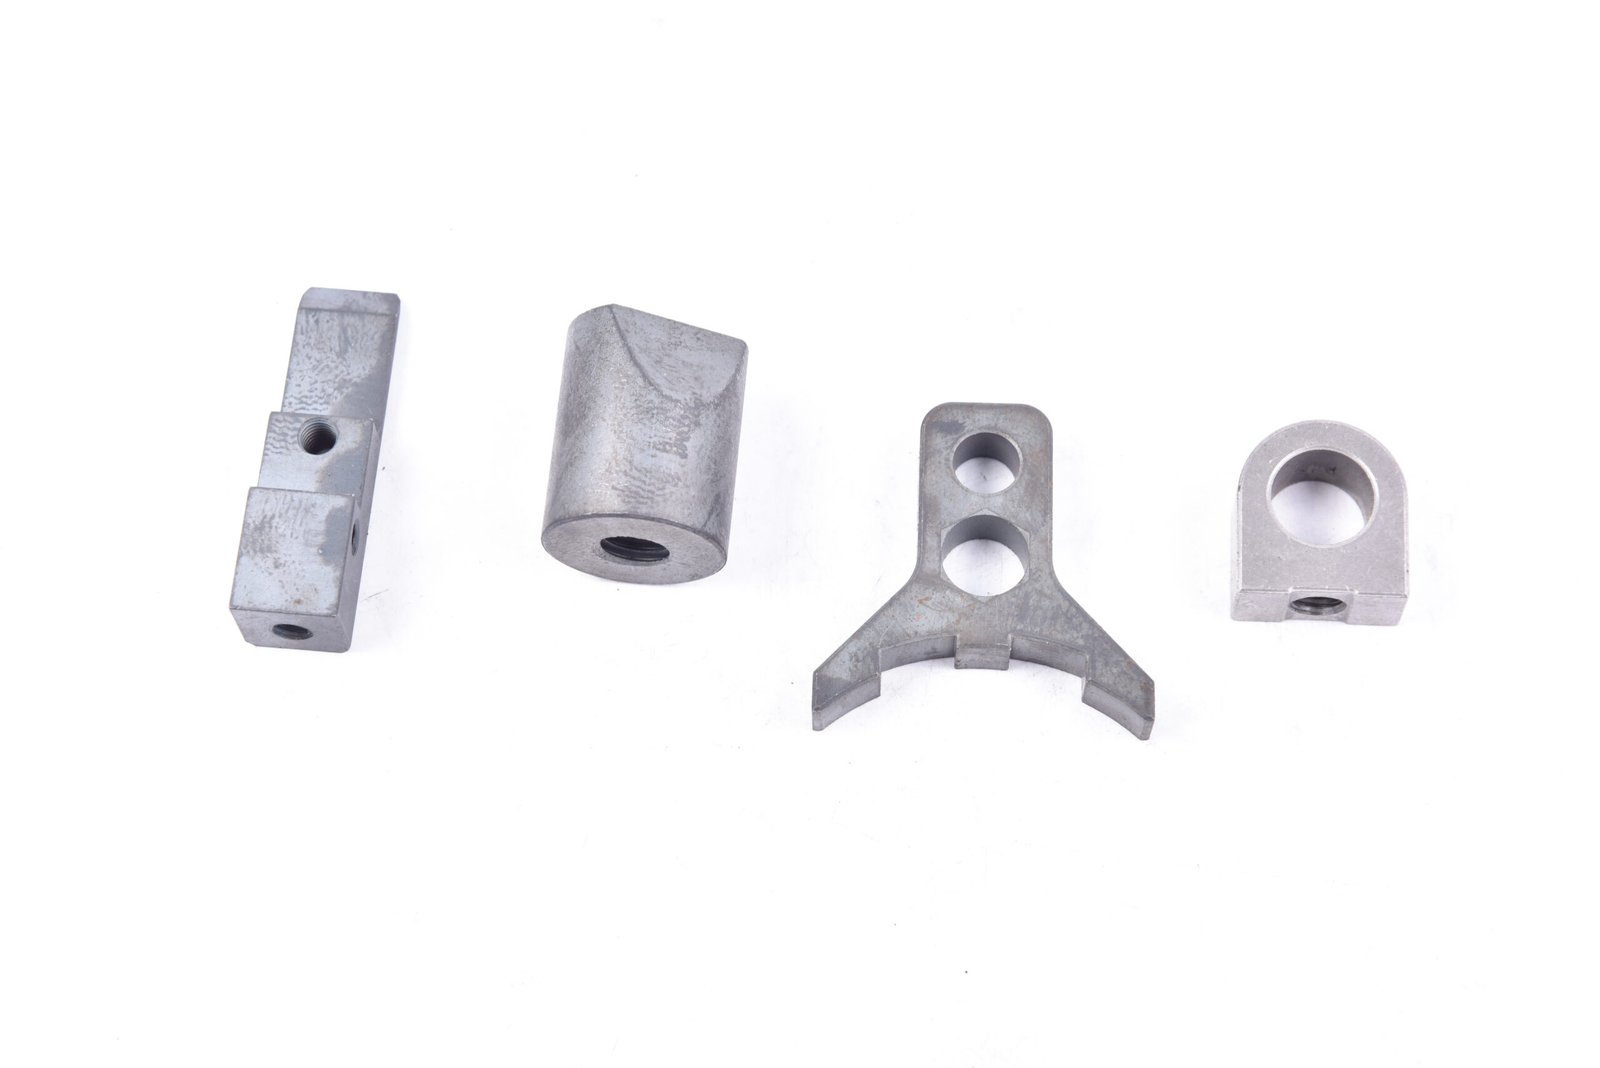
We make – PM is well-suited here
- Spur, helical and bevel gears for weaving and spinning machines
- Oil-impregnated bronze and iron bushings for self-lubricating housings
- Timing pulleys, sprockets and chain wheels for low-load drives
- Cams for shuttle, projectile and air-jet looms; valve actuators
- Spacer blocks, eccentric seats, thimble seats, rocker tables
- Lock nuts, washers, brackets – flat and small structural pieces
We don’t make – ask a partner shop
- Spindles, shafts, main frames, beating-up mechanisms (CNC / cast iron)
- Rubber-covered rollers and apron bars (rubber covering)
- Steel rings, cutters and blades (tool-steel CNC)
- Nozzles, ceramic thread guides, finished drives and inverters
Need CNC-machined or rubber-covered textile parts? Ask us anyway – we partner with CNC and rubber shops in Ningbo and can quote the full assembly under one PO. Tell us what you need.
Four part families we make for textile machines
Each cluster below groups the part geometries we run most often for weaving, spinning, knitting and dyeing lines. Click through to the part card for typical dimensions, materials and tolerances.
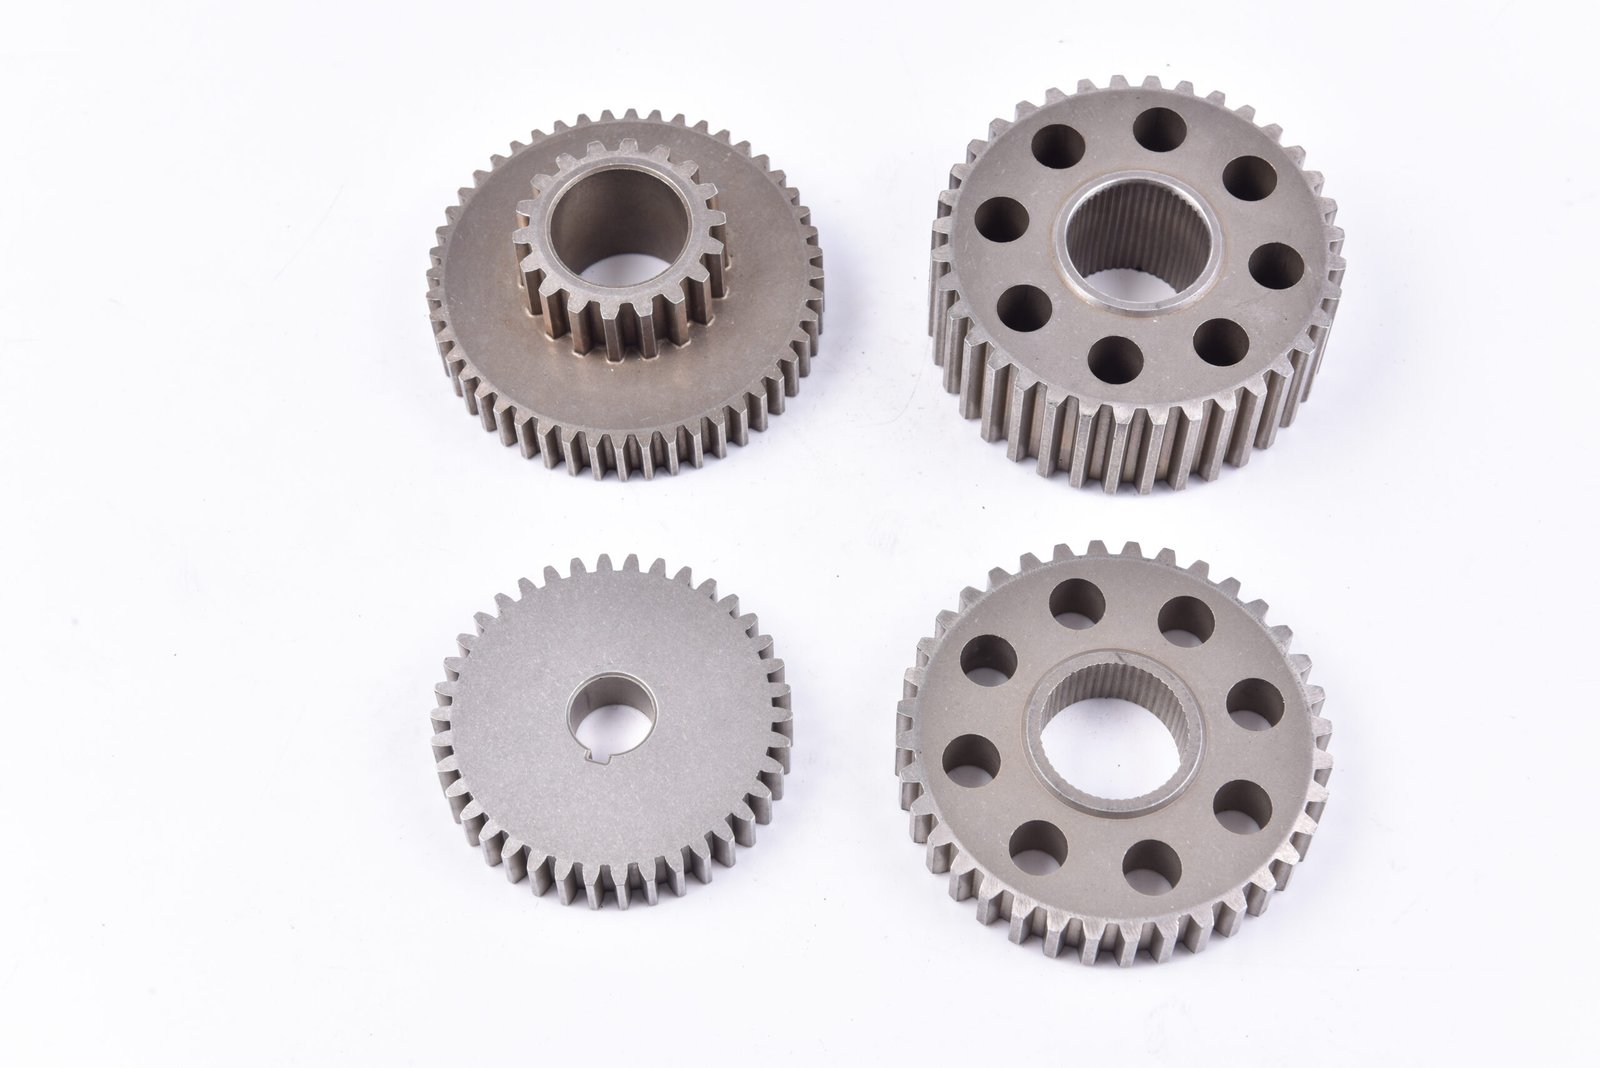
Sintered gears for textile machinery
Spur, helical, bevel and ring gears for weaving and spinning drives. Modulus 1.0-4.0, diameter up to 120 mm, density 6.8-7.1 g/cm³ on repressed gears.
Sintered bushings & self-lubricating bearings
Oil-impregnated bronze and iron bushings, flange bushings and thrust washers. 10-20% oil by volume; runs 3,000-5,000 hours without re-oiling.
Sintered transmission parts for textile machines
Timing pulleys, sprockets, chain wheels and cams for shuttle, projectile, rapier, air-jet and water-jet loom drives. Up to 60 teeth on pulley, single-row and duplex.
Sintered structural & accessory parts for textile
Spacer blocks, eccentric seats, thimble seats, rocker tables, lock nuts and brackets. Flat, small and geometrically simple – the natural fit for sinter forming.
Cluster 01 – Sintered gears for textile machinery
Spur, helical, bevel and ring gears used in transmission and shedding drives of weaving, spinning and knitting machines. We hold ISO JS7-JS8 on tooth profile and bore diameter, with density 6.8-7.1 g/cm³ on repressed gears – tighter than the DIN 6-8 typical of standard PM gear suppliers.
 Spur pinion gear for weaving & spinning drives
Modulus 1.0-3.0, OD up to 80 mm. Materials: Fe-Cu-C, Fe-Ni-Mo. Density 7.0+ g/cm³ after repressing.
 Helical pinion for spinning-frame drive
Helix angle 15-25°, modulus 1.5-3.5. Case-hardenable to HRC 55, suitable for continuous-duty motors.
Cluster 02 – Sintered bushings & self-lubricating bearings
Oil-impregnated sintered bushings are the workhorse of textile machines: they self-lubricate inside sealed housings, run quietly and survive the lint and humidity of a weaving shed. Our bronze and iron grades are sized against your existing sample or housing drawing, and we can match an existing P/N with a density and oil-content certificate.
 Oil-impregnated bronze bushing
Cu-Sn bronze, oil content 12-18% vol. OD 10-60 mm, length 8-50 mm. Pairs with spindles up to 3,500 rpm.
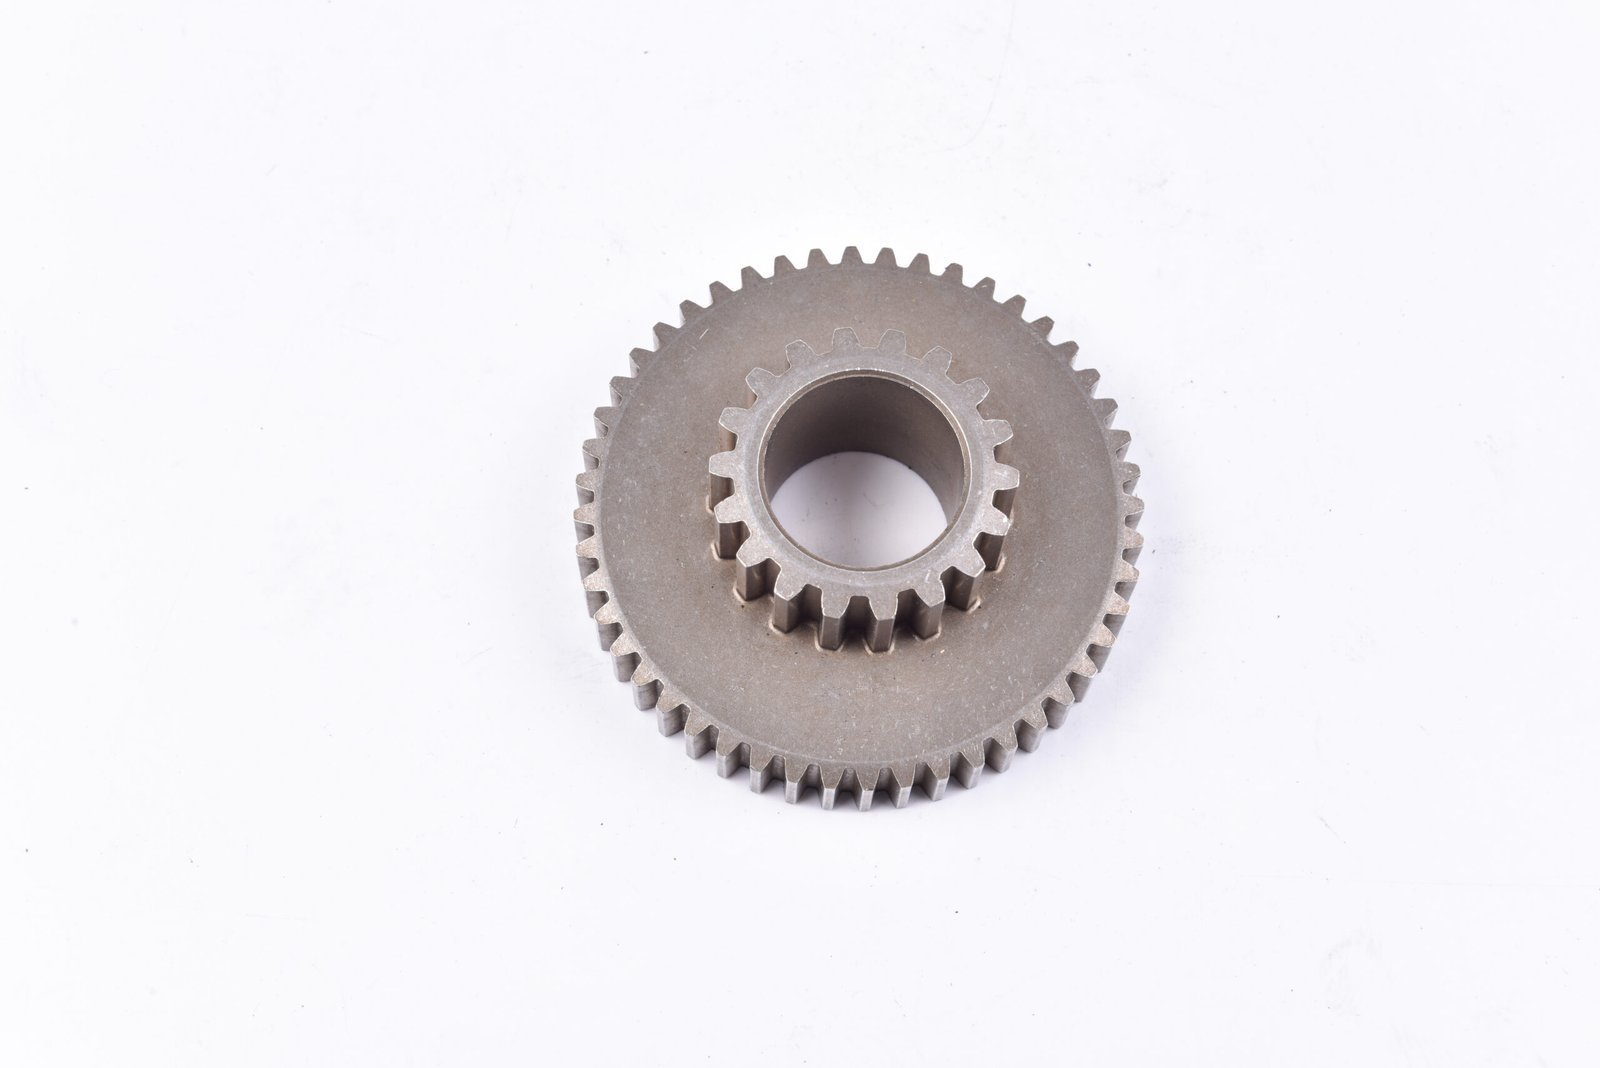 Flange bushing for spinning frame
Bronze or iron, flange OD 18-80 mm. Holds axial position; fits common ring-spinning and roving-frame housings.
Cluster 03 – Sintered transmission parts for textile machines
Timing pulleys, sprockets, chain wheels and cams. These run in the medium-load transmission chain of weaving, spinning and finishing machines. We supply them in 14-60 teeth counts with pilot bore, keyway, or pre-bored to your drawing.
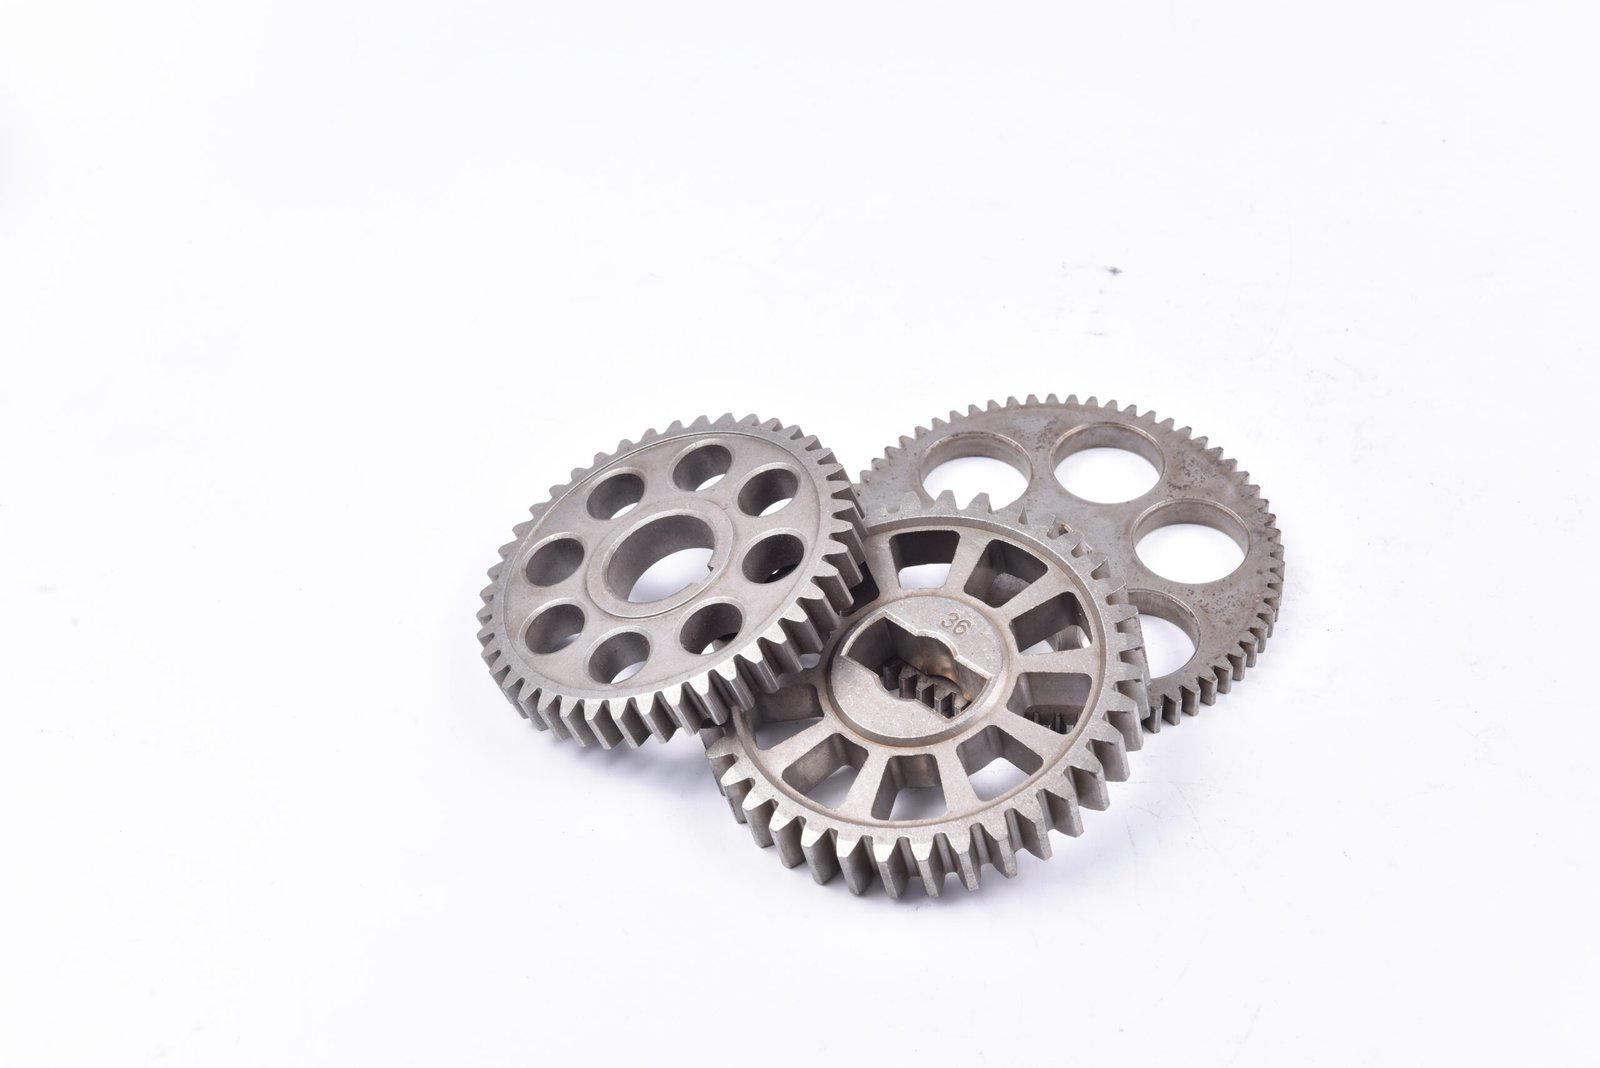 Sintered timing pulley for weaving machine
14-60 teeth, pilot bore or keyed. Re-pressed to 7.0 g/cm³ for tooth strength; suitable for HTD / T-type belts.
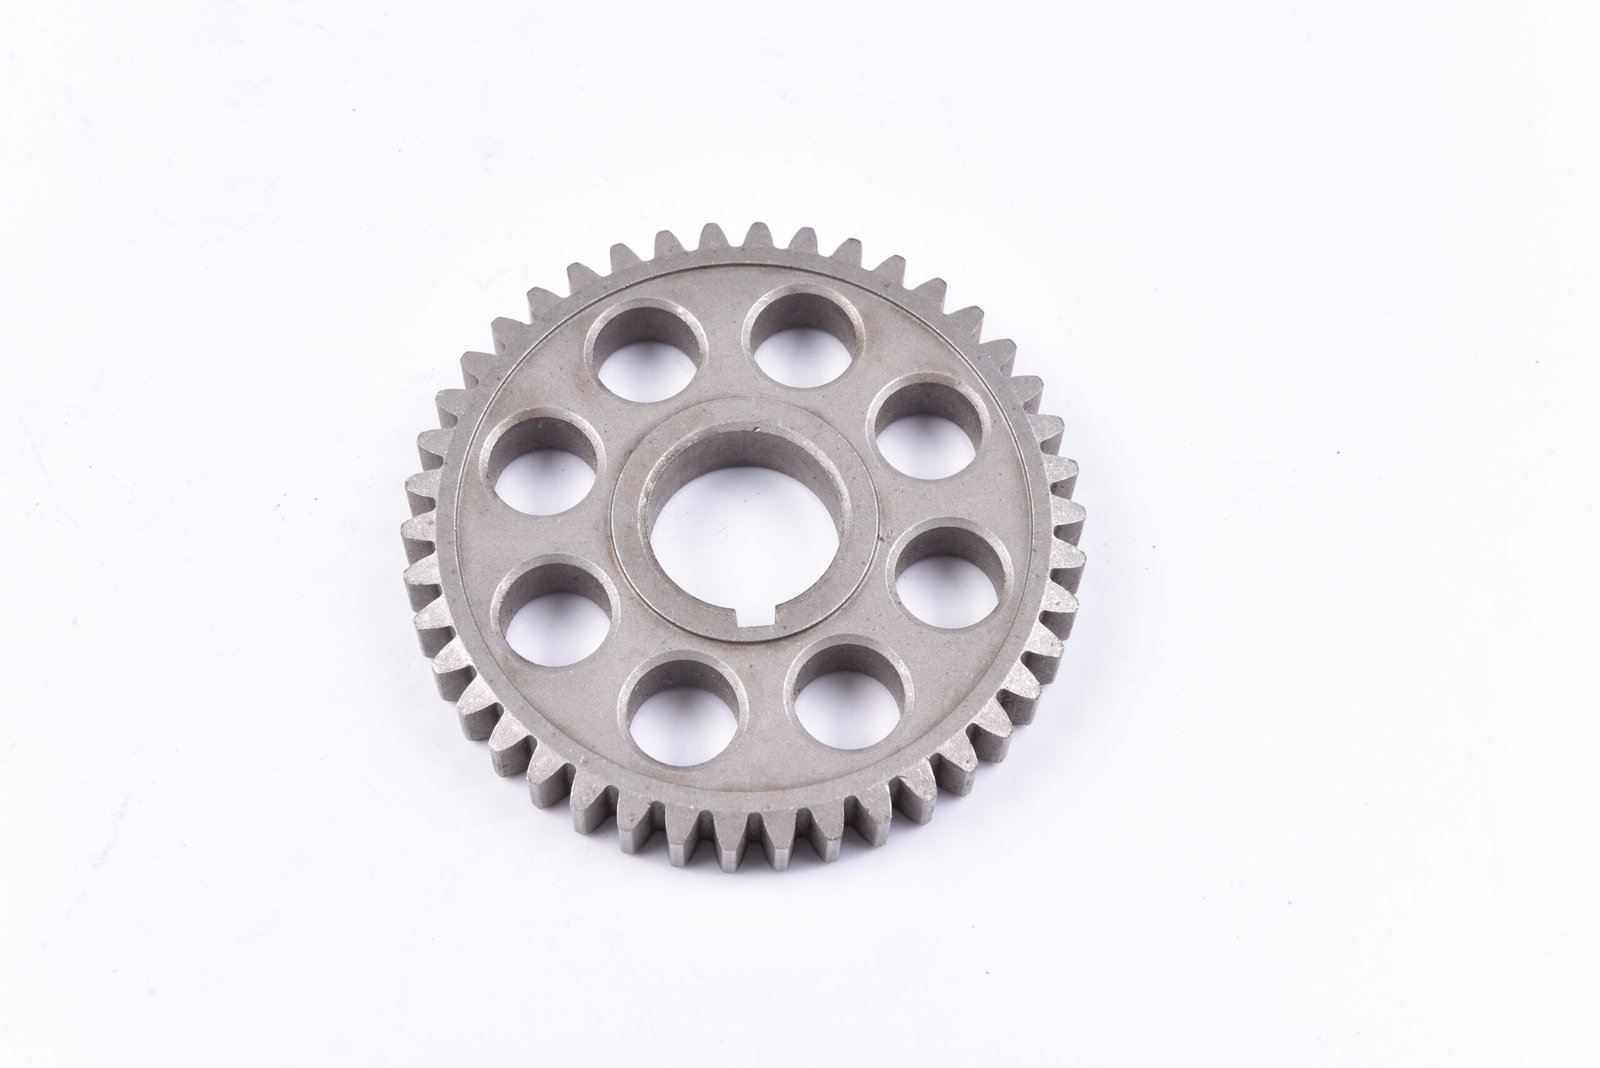 Sintered chain sprocket for spinning drive
14-30 teeth for 06B-12B simplex chain. Case-hardened to HRC 45 for wear resistance on the tooth flank.
Cluster 04 – Sintered structural & accessory parts for textile
Flat, small and geometrically simple parts where sinter forming shines: spacer blocks, eccentric seats, thimble seats, rocker tables, lock nuts and brackets. These are common wear items on weaving and spinning machines and a natural PM application.
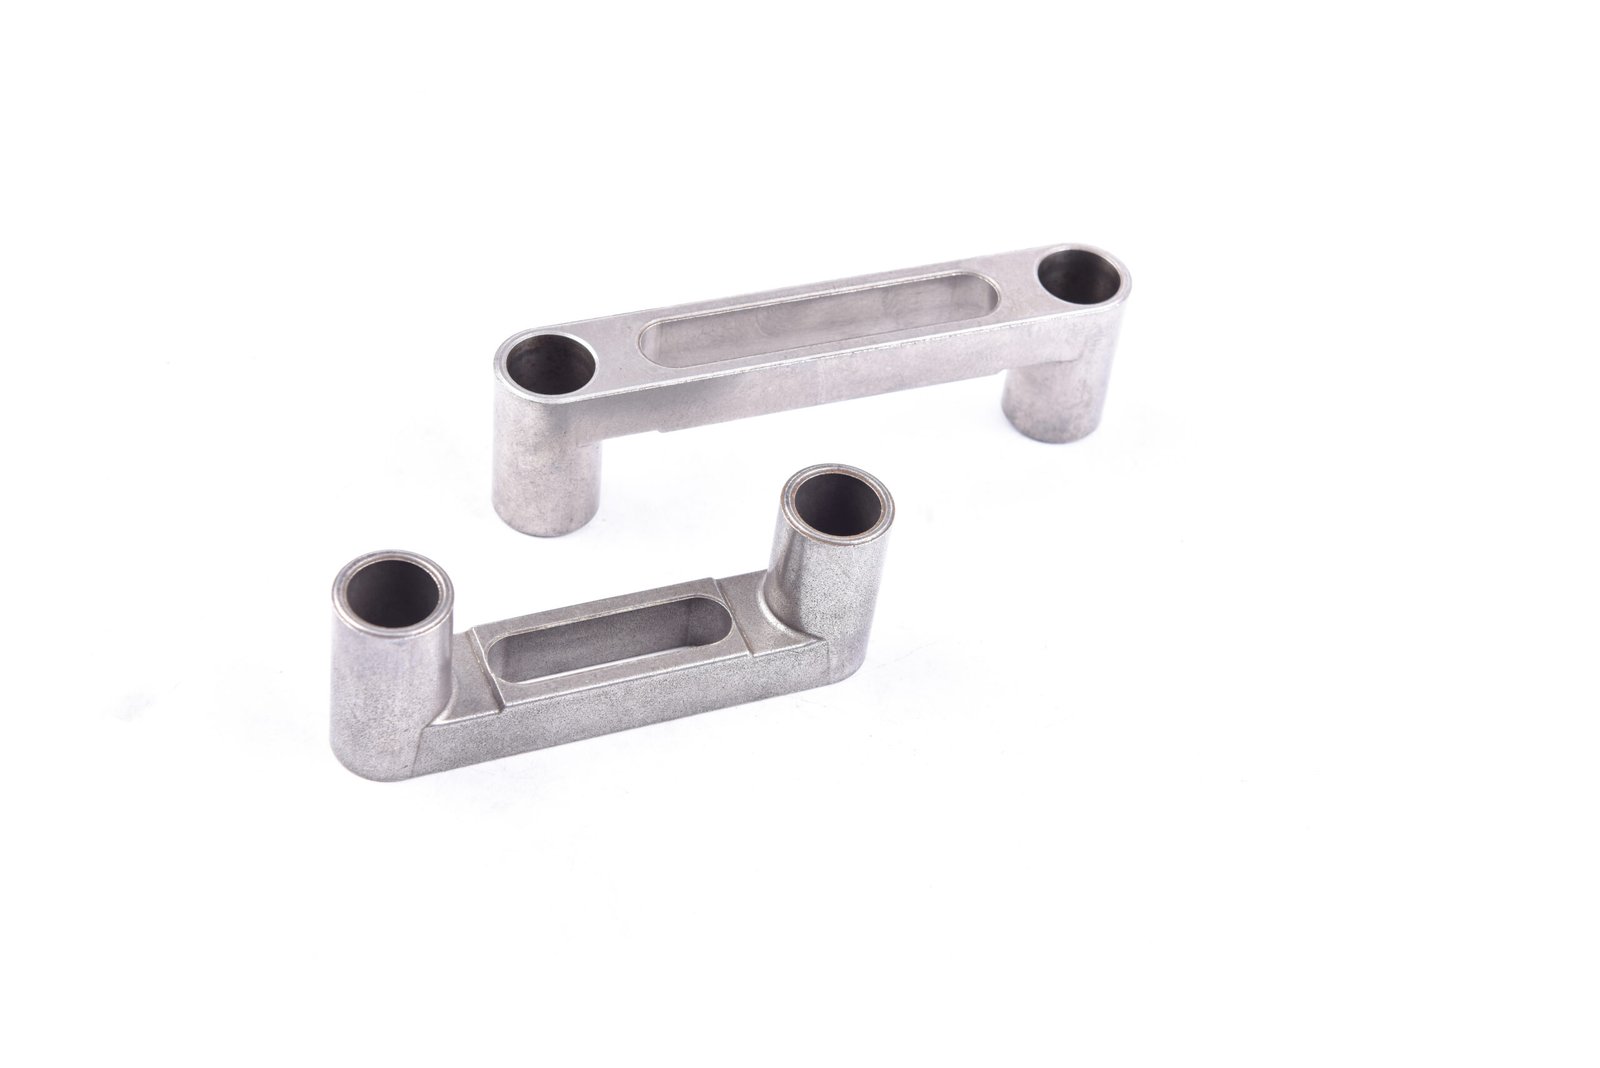 Spacer block for take-up mechanism
Flat block 10-80 mm footprint, 4-12 mm thick. Iron-based with copper infiltration for density stability.
Capabilities for sintered textile parts
What you can ask for in your RFQ. All numbers are in-house, not subcontracted.
| Parameter | Standard range | Notes |
|---|---|---|
| Materials | Fe-Cu-C, Fe-Ni-Mo, Fe-Cu, Cu-Sn bronze, stainless 316L / 17-4PH | Material certificate per lot |
| Density | 6.4 – 7.0 g/cm³ plain sinter; 7.0 – 7.2 g/cm³ repressed | Tested on every lot with in-house density meter |
| Hardness | HRB 60-90 plain; HRC 40-55 after steam / case hardening | Hardness tester per lot |
| Profile tolerance | DIN 6-8 (ISO JS8) plain; DIN 6 (ISO JS7) repressed | Zeiss CMM + gear profile tester |
| Maximum part footprint | approx. 120 mm in any direction | Matches 500 t PM press envelope |
| Surface treatment | Steam oxidation, oil impregnation, resin impregnation, copper infiltration | Selected per your drawing |
| MOQ | 2,000 pcs | Lower for sampling / replacement lots on request |
| Tooling lead time | approx. 20 days | In-house die design + EDM |
| Sample lead time | approx. 25 days after tooling approval | FAI report included |
| DFM review | 48 hours | Written DFM note against your drawing |
| QC | 3 Zeiss CMMs, gear profile tester, density & hardness tester | Lot-level MES traceability |
| Certifications | IATF 16949 : 2016, ISO 9001 : 2015 | Audited annually by SGS |
| Common HS code | 7326 (other articles of iron/steel) / 8483 (transmission parts) | For customs declaration |
How a sintered textile part is made at JH PM
Six steps from your drawing to a traceable lot. Same process we use for automotive and power-tool gears – textile fits the same PM line.
FAQ – Sintered parts for textile machinery
Which sintered parts fit weaving and spinning machines best?
Sintered PM parts work best for low-to-medium-load transmission and self-lubricating parts on weaving, spinning, knitting and dyeing machines: spur, helical and bevel gears, timing pulleys, sprockets, oil-impregnated bushings and flange bushings, cams for shuttle and projectile looms, spacer blocks, eccentric seats and thimble seats. They are not the right process for high-speed spindles, main frames, beating-up mechanisms or rubber-covered rollers – those go through CNC machining, casting or rubber covering.
What density and hardness can you hold on sintered textile parts?
Standard sintered iron and Fe-Cu-C parts reach 6.4-7.0 g/cm³ density; we hold 7.0+ g/cm³ on high-load gears by repressing and refiring. Surface hardness runs HRB 60-90 on plain sinter, HRC 40-55 after steam oxidation or quench-hardening on tooth surfaces, with case depth 0.3-0.8 mm on carburised gears. Density and hardness are tested on every lot with our in-house density meter and hardness tester before shipment.
Can you hold the tolerances weaving machine gears need?
Yes – on tooth profile, bore diameter and runout we routinely hold ISO JS8 on plain sinter and ISO JS7 on repressed gears, which is tighter than the DIN 6-8 typical of competitors. Critical dimensions such as timing-pulley tooth-to-tooth spacing are checked with our gear profile tester against your drawing; we share the FAI report before serial production.
Do you supply oil-impregnated bushings for spinning frames?
Yes. Oil-impregnated sintered bronze and iron bushings are a flagship product for our textile customers. Oil content runs 10-20% by volume, so the bushing self-lubricates for the first 3,000-5,000 running hours without re-oiling – which is why most spinning-frame and ring-spinning retrofitters specify PM bushings instead of machined bronze. We can match an existing bushing from a sample, or design a new one against your housing drawing.
What is the typical MOQ and lead time for a sintered textile part?
MOQ starts at 2,000 pieces – useful for mid-volume spares and aftermarket programs. Tooling takes around 20 days; first-article samples are delivered in about 25 days after tooling approval. For urgent breakdown spares we keep a small buffer of common gear and bushing geometries; ask for a stock check on your part number.
Which loom brands are your parts commonly fitted to?
Our sintered gears, timing pulleys, cams and bushings are used in spare-part programs for the major loom families – Toyota JAT810, Tsudakoma, Picanol Optimax and GTM, Itema R9500 and Leonardo, Sulzer G6200, Somet Thema, and rapier / projectile / air-jet / water-jet looms in general. We also supply spinning-frame and knitting-machine parts where the geometry is suitable for PM.
Have a textile part in mind?
Send a drawing and get a DFM review within 48 hours. We make PM gears, bushings, timing pulleys, cams and small structural parts for weaving, spinning, knitting and dyeing machines. For CNC-machined or rubber-covered items, ask us anyway – we partner with CNC and rubber shops in Ningbo.
Request a Quote