Sintered Metal Parts — Custom Press-and-Sinter Manufacturing
Sintered metal parts are components made by compressing metal powder in a die under high pressure, then heating it below the melting point so the particles bond into a solid, near-net-shape part. The press-and-sinter process delivers strong, dimensionally stable parts — gears, structural components, bearings and more — at a lower cost per piece than machining, with self-lubricating options available.
We are the factory, not a middleman: powder blending, pressing, sintering, finishing and Zeiss inspection all run inside our own 30,000+ m² facilities. Send a drawing and get a DFM review plus quotation within 48 hours.
Custom sintered parts, by material & application
Five product families cover the majority of press-and-sinter demand. If your part is not on the list, send the drawing anyway — as a custom sintered parts manufacturer we quote against geometry, not catalogue lines.
Sintered Iron Parts
Structural components, lock components, housings and mounting parts in iron and low-alloy steel — load-bearing parts that need strength at competitive cost.
iron · steelSintered Steel Gears
Spur, helical, bevel, worm and timing gears from powder compaction — near-net gear teeth mean no chip removal and no material waste.
gears · sprocketsSintered Stainless Parts
Corrosion-resistant components in stainless steel 304L, 316L and 430 — for industrial, automotive and end-user-facing parts that must stay clean.
304L · 316L · 430Sintered Bronze Bearings
Oil-impregnated, self-lubricating bearing bushings and flanged bearings — the classic press-and-sinter application for friction-free assemblies.
self-lubricatingThe press-and-sinter process, in five steps
A compressed version of the full powder metallurgy route — enough to understand cost drivers, tolerances and lead time.
Powder blending
Alloy powder, lubricant and additives are blended to the target composition for your material spec.
Compaction
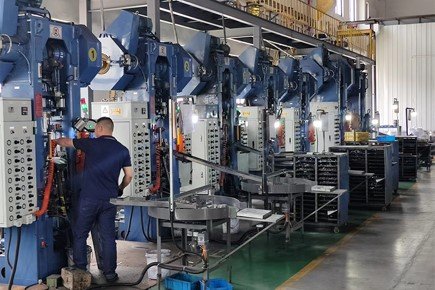
Powder is pressed in a die under high pressure on one of 19 PM presses into a raw “green” part.
Sintering
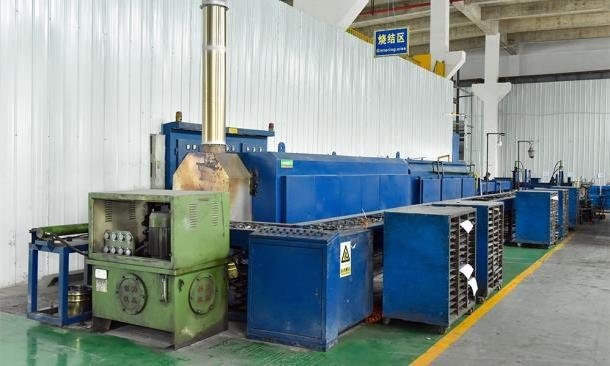
Green parts are heated in 10 controlled-atmosphere furnaces so particles bond into solid metal.
Sizing / CNC
Optional sizing or CNC finishing tightens critical dimensions down to ±0.025 mm.
Inspection & ship
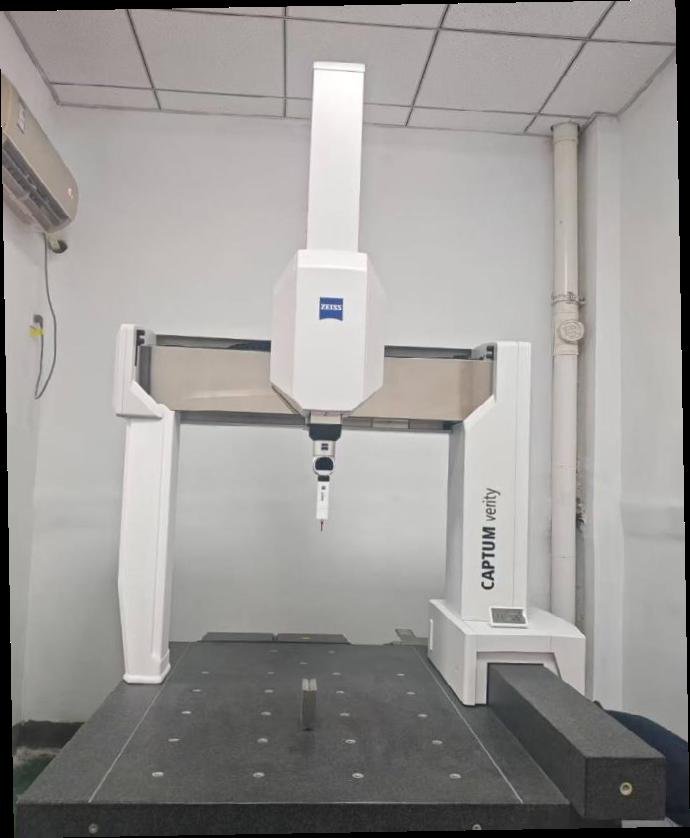
Zeiss CMM, density testing and batch traceability through MES — PPAP/FAI documentation on request.
Want the full technical background — densification, tolerances, design rules?
Read the complete powder metallurgy process guide →See the sintered metal parts factory in China
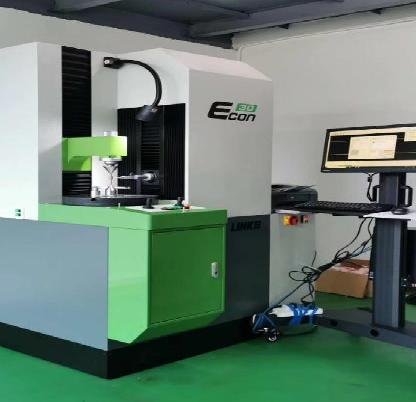
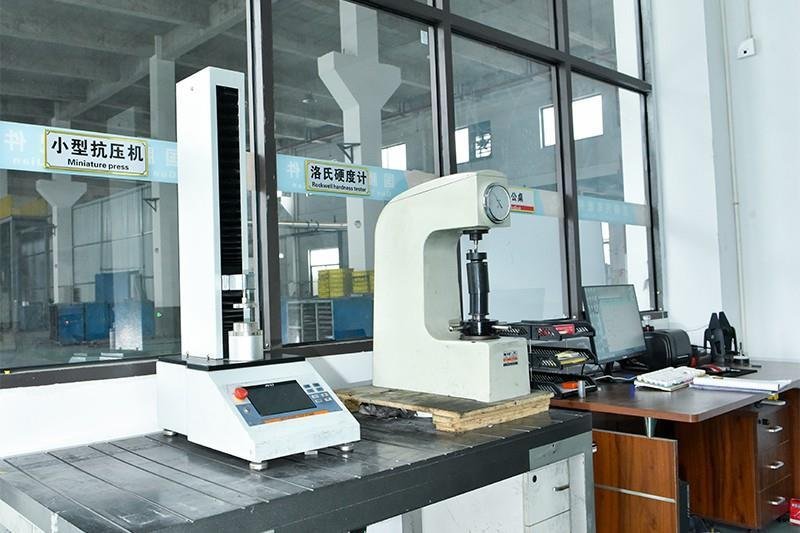
Buyers searching for a sintered parts factory in China want to see the shop floor, not a brochure. This is ours: presses, furnaces, inspection — in Shaoxing, China.

What we can quote against
The numbers engineers actually ask for. Final values are confirmed per part in the DFM review — no guessing.
| Parameter | Capability | Notes |
|---|---|---|
| Materials | Iron · carbon steel · stainless steel (304L, 316L, 430) | Bronze alloys available for project-specific applications. |
| Part size | Up to ≈120 mm outer diameter (projection-area limited) | Depends on geometry and required density — confirmed at DFM. |
| Tolerances | ±0.05 mm standard · ±0.025 mm after sizing & CNC | Key dimensions; depends on geometry and feature type. |
| Sintered density | Iron 6.6–7.2 · Steel 6.8–7.4 · Stainless 6.9–7.6 g/cm³ | Typical MPIF ranges; target density per application. |
| Volume | MOQ 2,000 pcs · pilot batches available | Low-MOQ friendly for new-product ramp-ups. |
| Capacity | 3,000+ t/yr (≈250 t/month) | 19 PM presses · 10 sintering furnaces · 2 continuous furnaces. |
| Quality | IATF 16949:2016 · ISO 9001:2015 | PPAP · FAI · MES batch traceability · 3× Zeiss CMM. |
| Lead time | Tooling ≈30 days · first articles ≈25 days | Quotes and DFM feedback within 48 hours of drawings. |
* Density and hardness values are typical industry ranges for press-and-sinter; exact targets depend on material and application and are locked in during the DFM review.
** EU shipments: our packaging supports PPWR (EU 2025/40) compliance documentation on request.
Why engineers route their sintered parts here
Six reasons this page is worth a quote, stated as straight facts.
Factory, not trader
Blending, pressing, sintering, finishing and inspection all inside our 30,000+ m² plants. One chain of custody, no middleman margin.
Automotive-grade quality
IATF 16949:2016 and ISO 9001:2015. PPAP, FAI and material certificates on request — documentation that passes customer audits.
Breadth of equipment
19 PM compaction presses, 10 sintering furnaces, 2 continuous furnaces, plus CNC and 3× Zeiss CMM — in-house at every stage.
PM + MIM under one roof
Complex micro-features? We switch to MIM when press-and-sinter hits its geometry limit — you get the right process, not the one we happen to own.
48-hour DFM review
Send a CAD and we flag tooling risks, draft angles and tolerance issues before you spend a dollar on tooling.
60+ countries, EU & US focused
PPWR-compliant packaging documentation, English-speaking project engineers, and a track record with European and North American OEMs.
Sintered metal parts — questions buyers ask
What are sintered metal parts?
How does press-and-sinter manufacturing work?
What materials can you sinter?
What tolerances can you hold on sintered parts?
What is the MOQ for sintered metal parts?
How fast is tooling and first article delivery?
Are you a sintered parts manufacturer or a trader?
Do you provide PPAP and quality documentation?
Send a drawing. Get a DFM review in 48 hours.
Email your CAD or PDF to our project engineers. You will receive a manufacturing review — material fit, tolerance feasibility, tooling cost and per-piece price — within two working days. No obligation, no guessing.